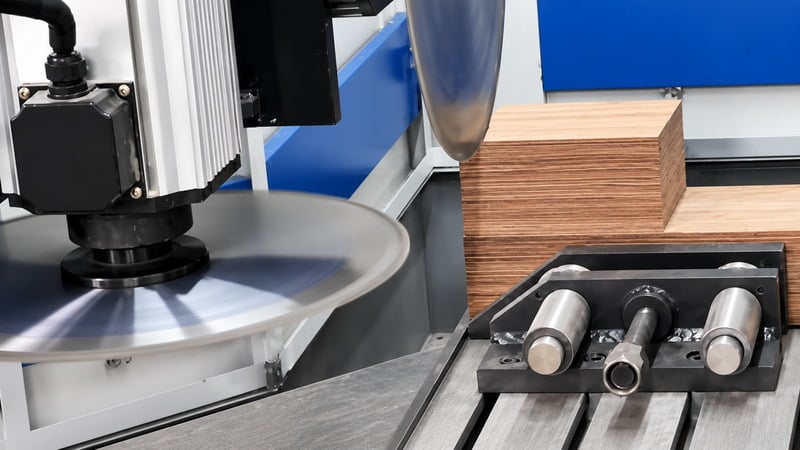
Step blocks were subcontracted and hand-milled with burnt surfaces. CNC coordinate machining now runs the cycle at ±0.3 mm, no polishing needed.
TRANFOVIA(NINGBO) EQUIPMENT TECHNOLOGY CO.,LTD

Step blocks were subcontracted and hand-milled with burnt surfaces. CNC coordinate machining now runs the cycle at ±0.3 mm, no polishing needed.
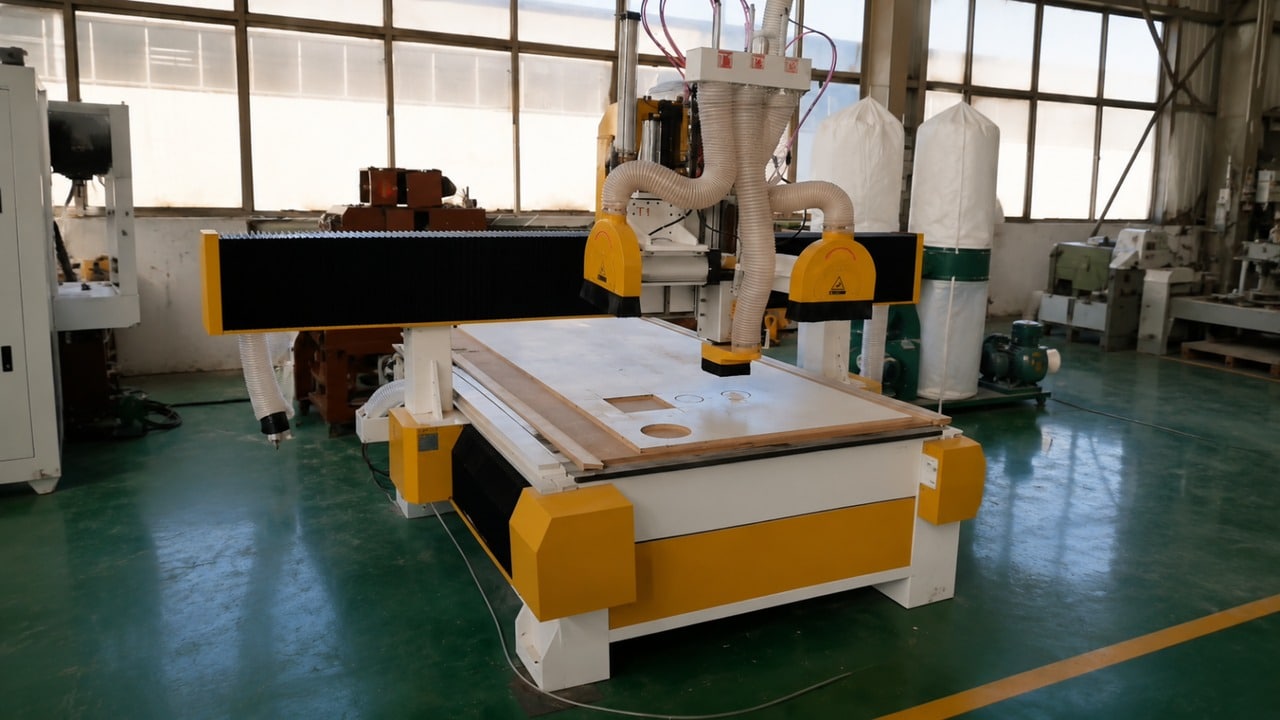
End rings were bought in and set out by hand, so lead time and concentricity both drifted. One platform now mills, grooves and drills per clamping.
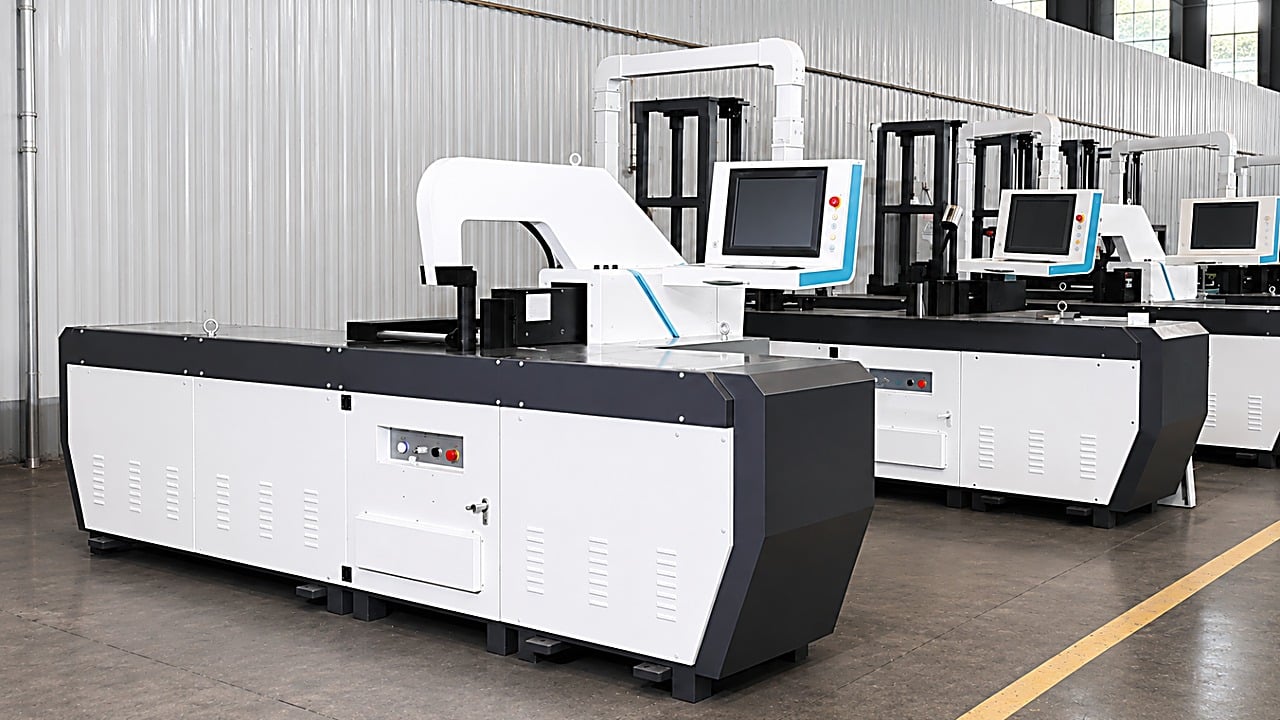
Servo CNC Busbar Bending Machine Holds ±0.3° Angle and ±0.15 mm Position on 15 × 200 mm Copper
A Kuala Lumpur switchgear maker replaced manual busbar bending with a servo CNC machine — ±0.15 mm stopper position, ±0.3 angle, program-based size changes on 15 × 200 mm copper.
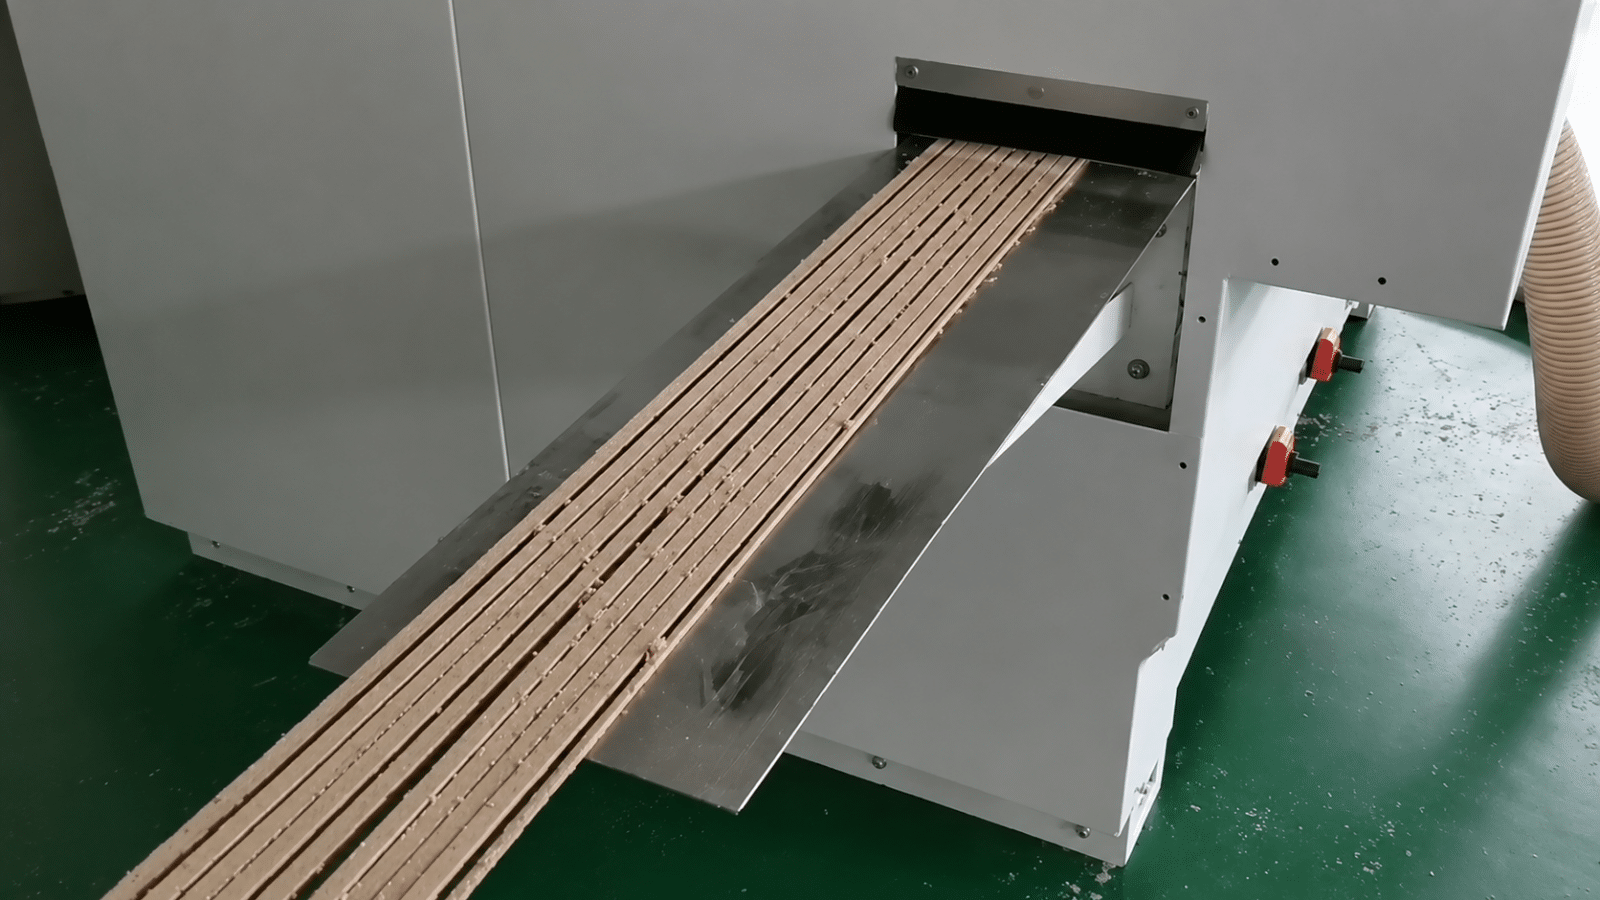
A transformer insulation parts workshop in Algiers replaced single-strip shaping with a multiple strips shaping machine — 10–20 strips per feed, ~5× efficiency, 20% less pressboard waste.
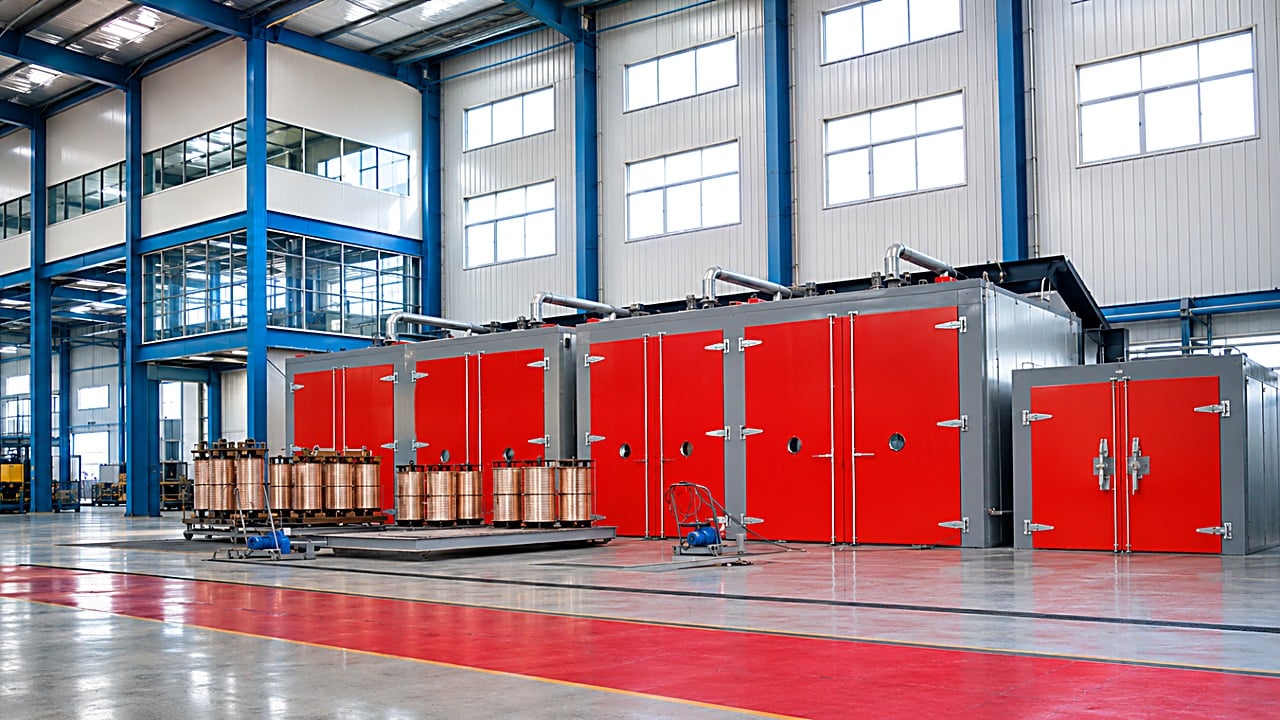
HB Series Curing Oven for Transformers in Tashkent, Uzbekistan
Manual heating left curing cycles unrepeatable and unrecorded. PID-programmed curing now holds ≤±2.5°C uniformity with a traceable curve.
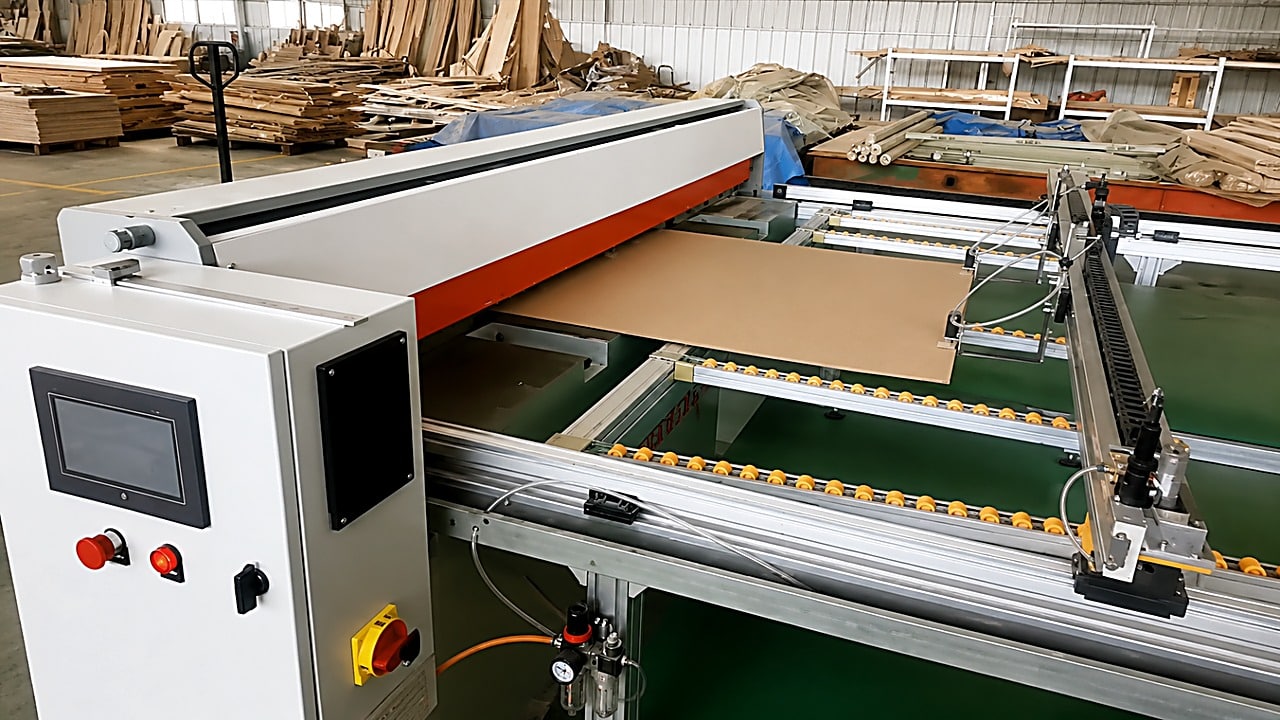
CNC Pressboard Shearing Machine at an Insulation Parts Workshop in Casablanca, Morocco
Manual layout and shearing left strip widths and oblique end-ring angles unstable. NC feeding now holds 0.2 mm tolerance on both strip types.
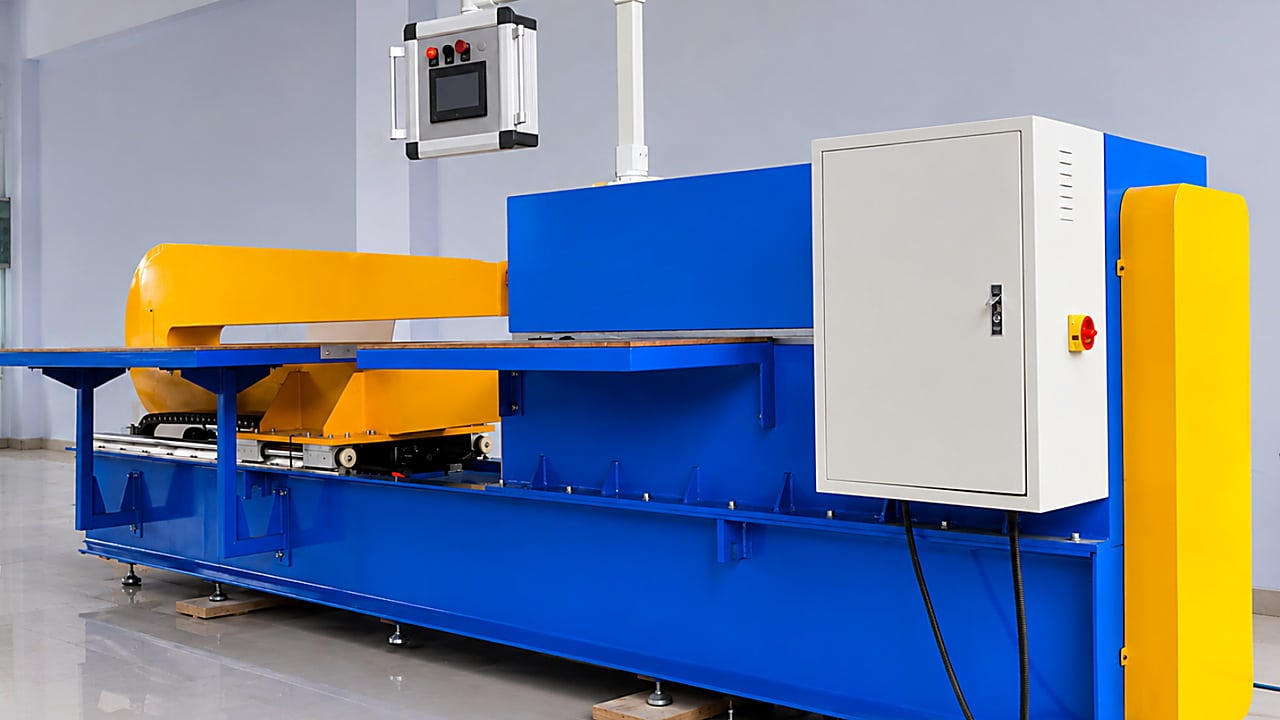
Pressboard Circular Shearing Machine at a Distribution Transformer Plant in Lagos, Nigeria
A Lagos transformer plant replaced manual pressboard ring cutting with the YJΦ300-2000 CNC circular shearing machine — holding ±1 mm ellipticity on Ø300–2000 mm end rings and angle rings, with burr-free edges.

Silicon Steel Slitting Line at a Transformer Core Shop in Dhaka, Bangladesh
Outsourced slitting left strip width, burr and lead time to others. One pass holds 0.02 mm burr on 40–1200 mm strips from a 10 T master coil.
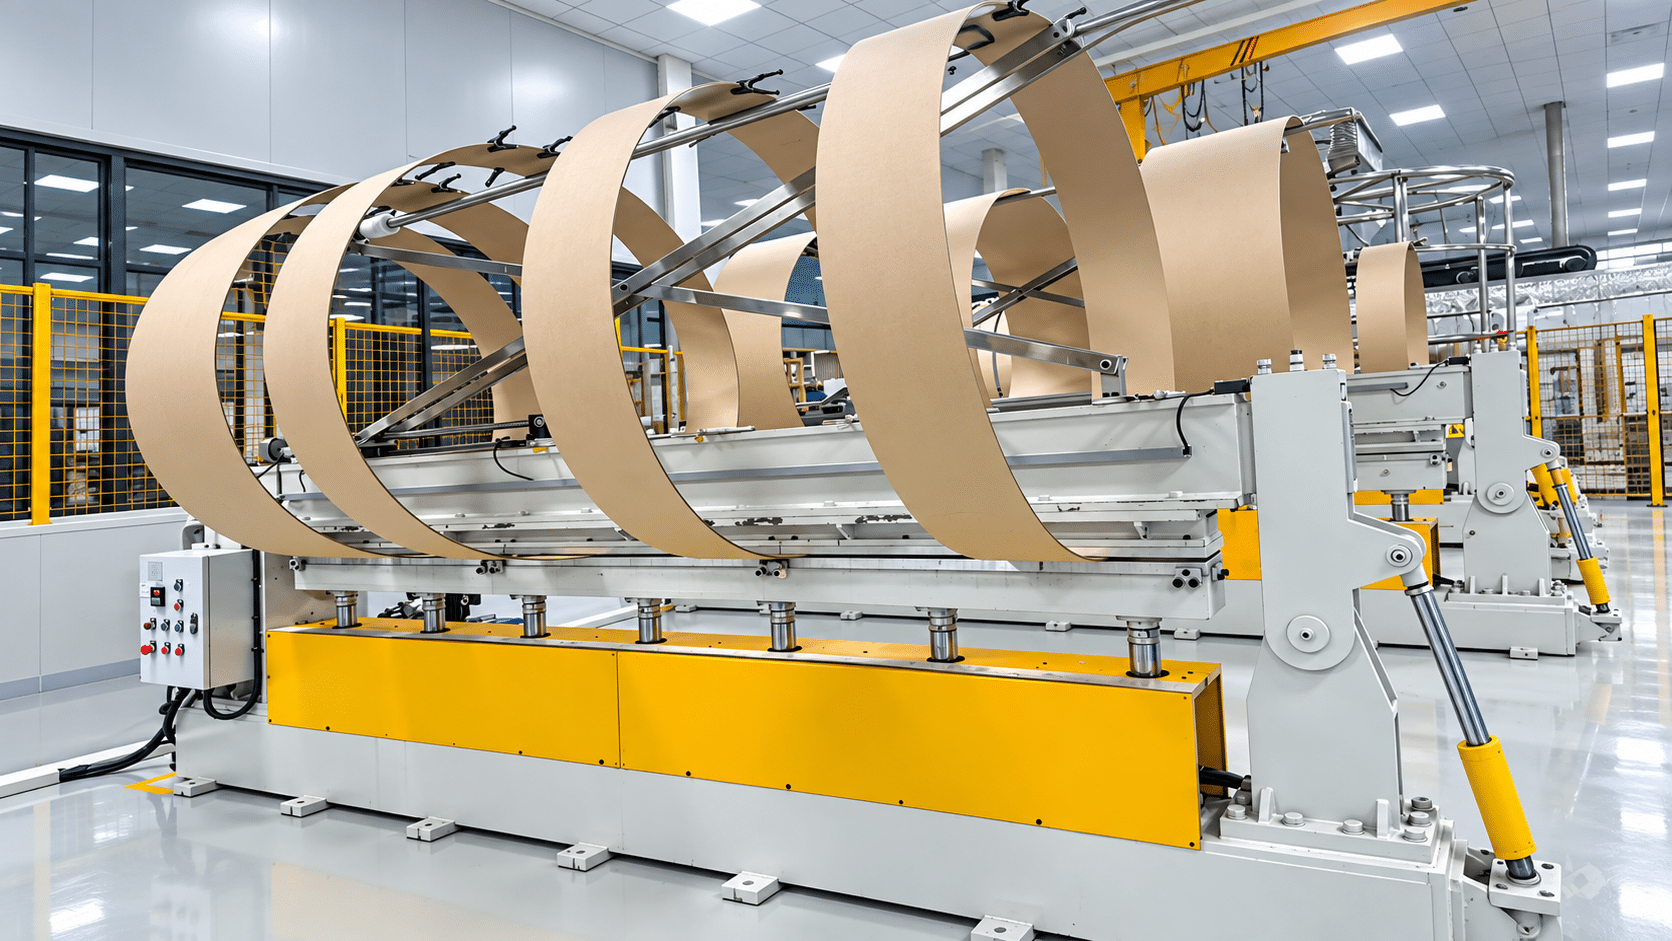
Outsourced beveling, hand-held rolling and air-drying left lap thickness drifting. One line now ties all three steps to a single parameter set.

