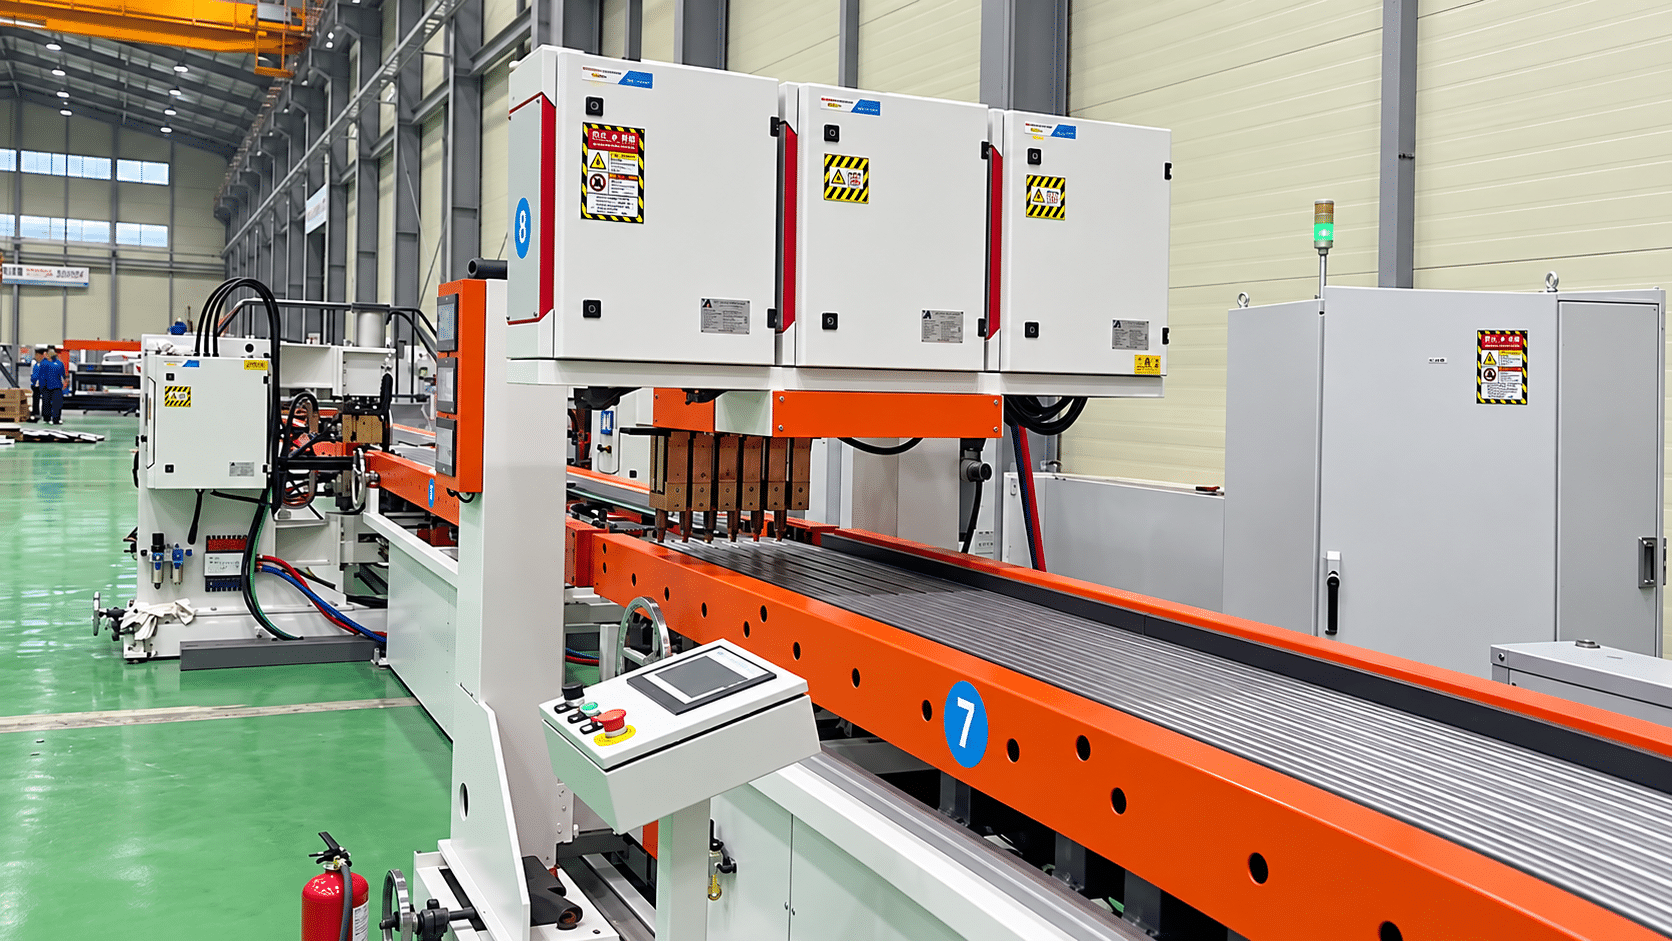
Transformer Radiator Production Line: High-Tempo Stable Output at a Korean Radiator Manufacturer
Tempo depended on people and weld appearance swung by batch. Programmed parameters fixed both: 60–75 panels/hour, uniform welds, no broken flow.
TRANFOVIA(NINGBO) EQUIPMENT TECHNOLOGY CO.,LTD

Transformer Radiator Production Line: High-Tempo Stable Output at a Korean Radiator Manufacturer
Tempo depended on people and weld appearance swung by batch. Programmed parameters fixed both: 60–75 panels/hour, uniform welds, no broken flow.
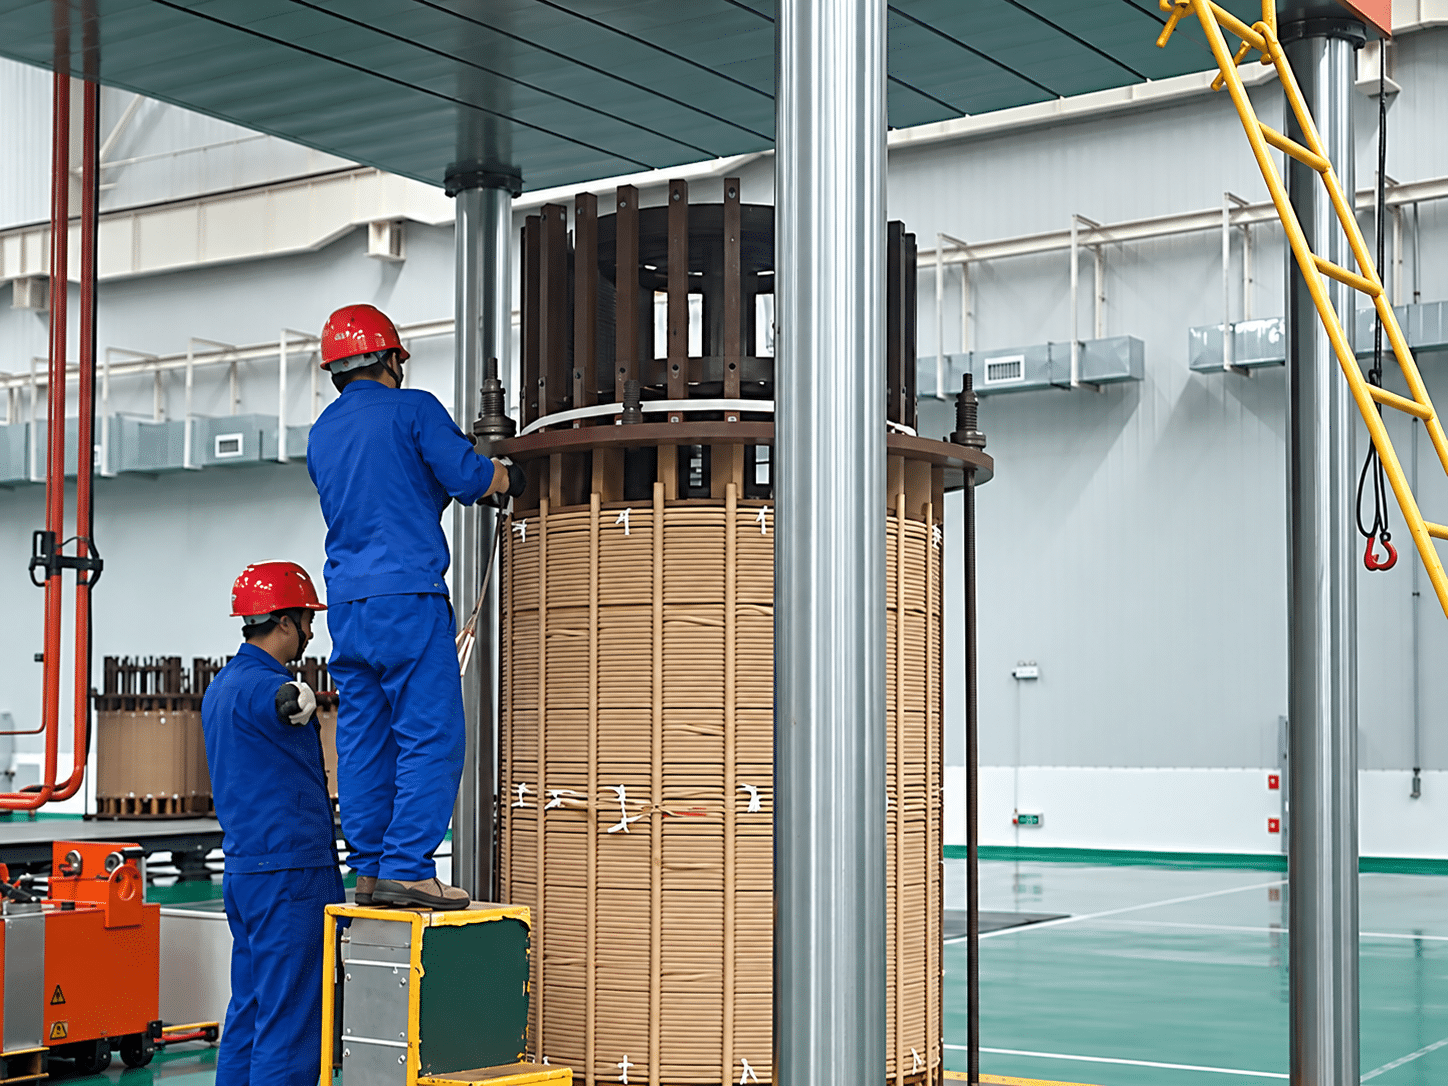
For high-mix small-batch coils, program-based pressing and fast changeover tightened height to ±1.2 mm and cut per-coil time to under 10 minutes.
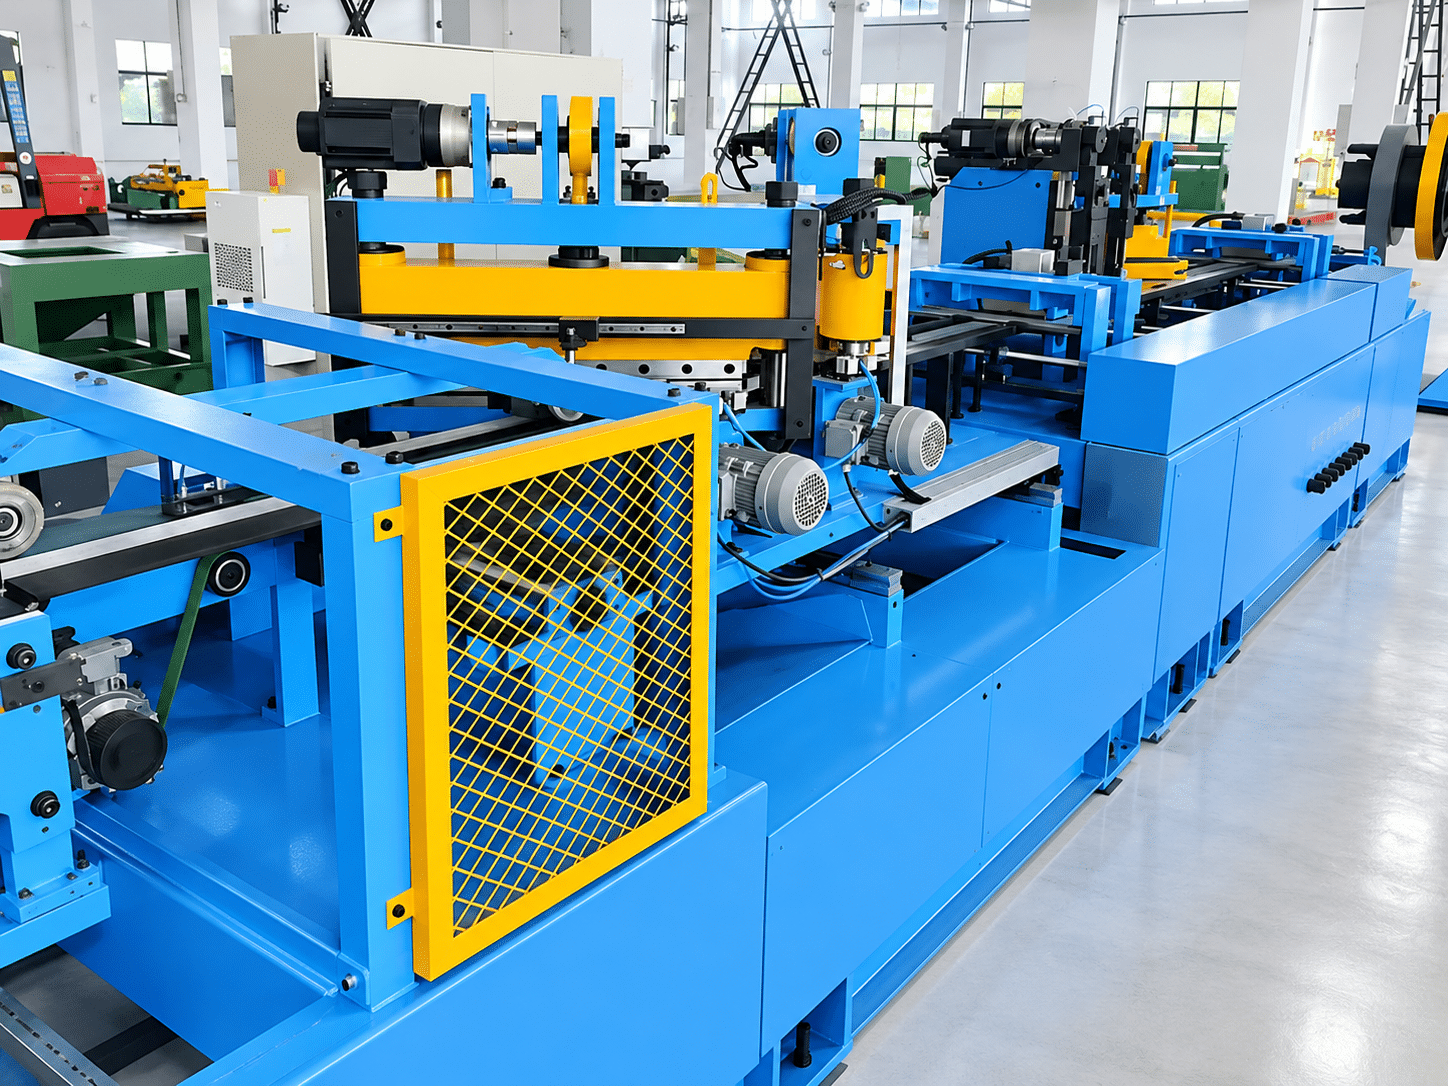
Laminations once depended on manual feel and burr was hard to control. Automatic feeding and cut-to-length shearing now hold accuracy at ±0.05 mm/m.
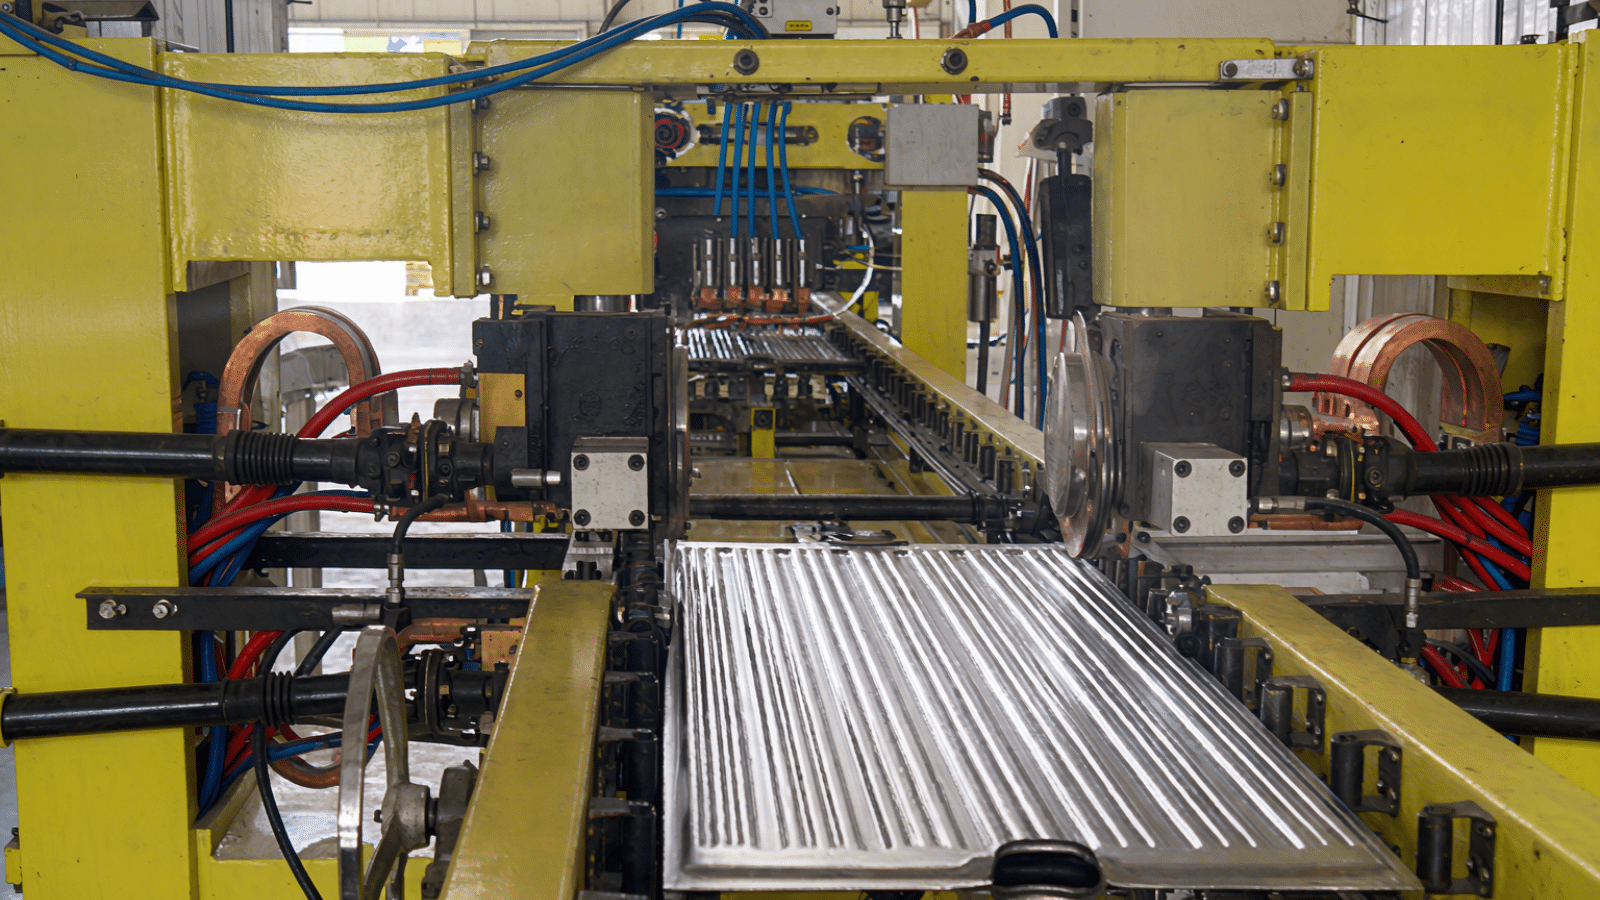
Scattered stations, feel-based welding and slow changeovers once slowed this shop. One programmed line now runs from coil to stack with 1–2 operators.
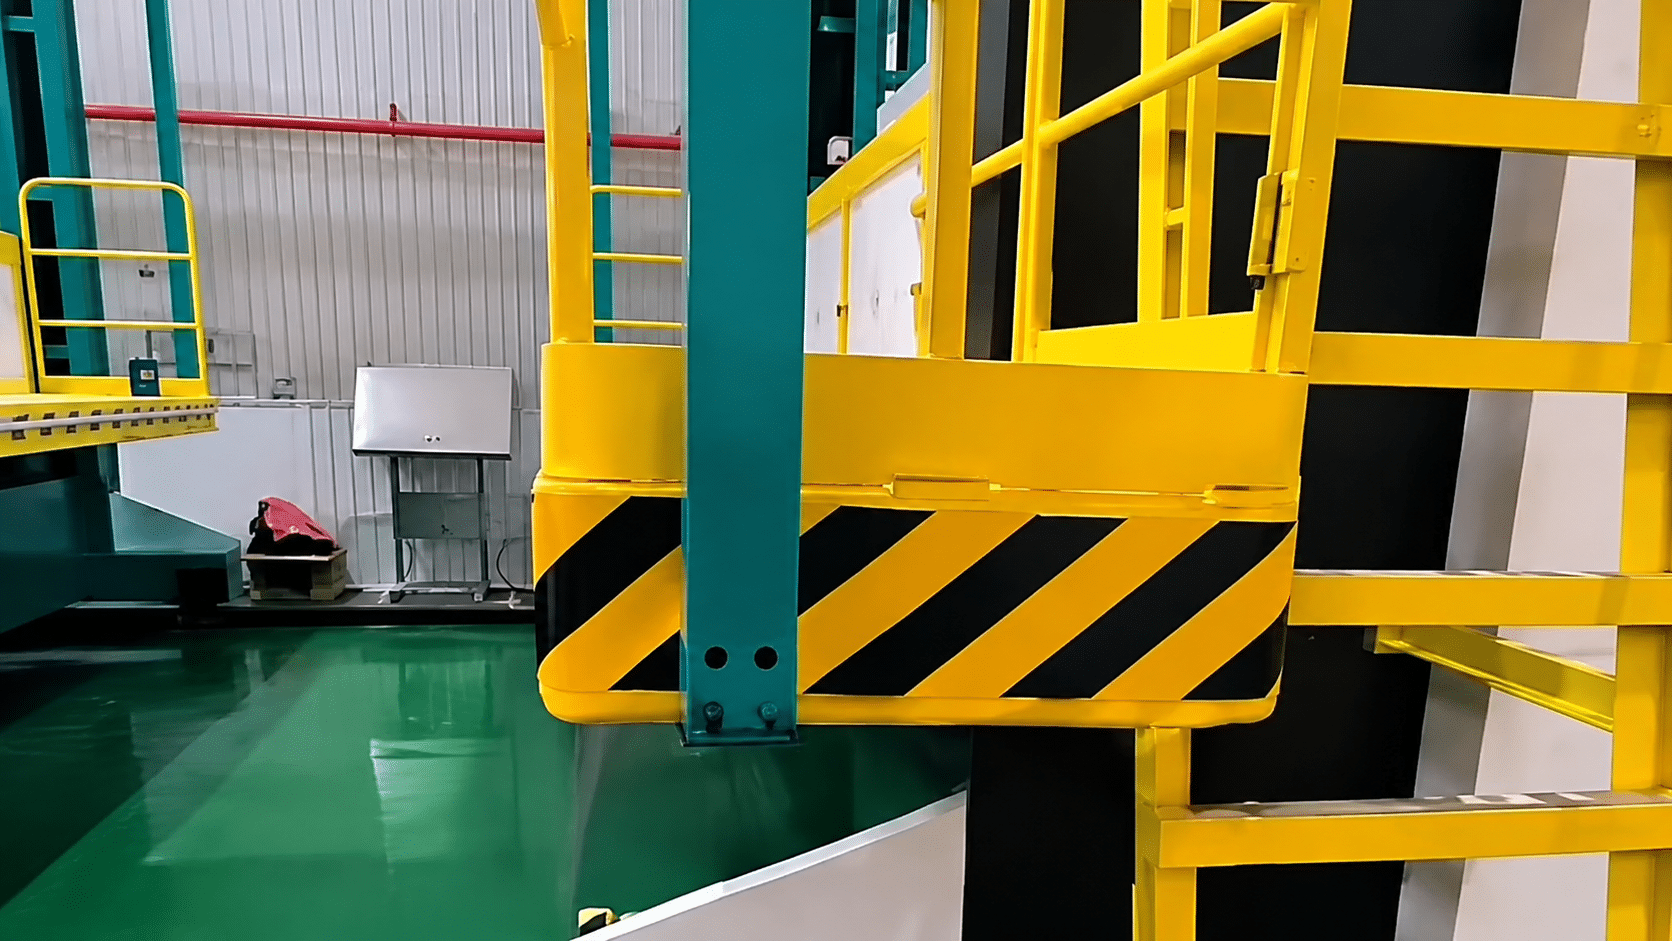
Assembly Platform Case Study: Omani Power Transformer Manufacturer Cuts Assembly Time by Half
Body-assembly bottlenecks, commissioning, and three-month results: cycles down to 1-1.5 days, crews of 4-5, 80% fewer temporary cords and lights.
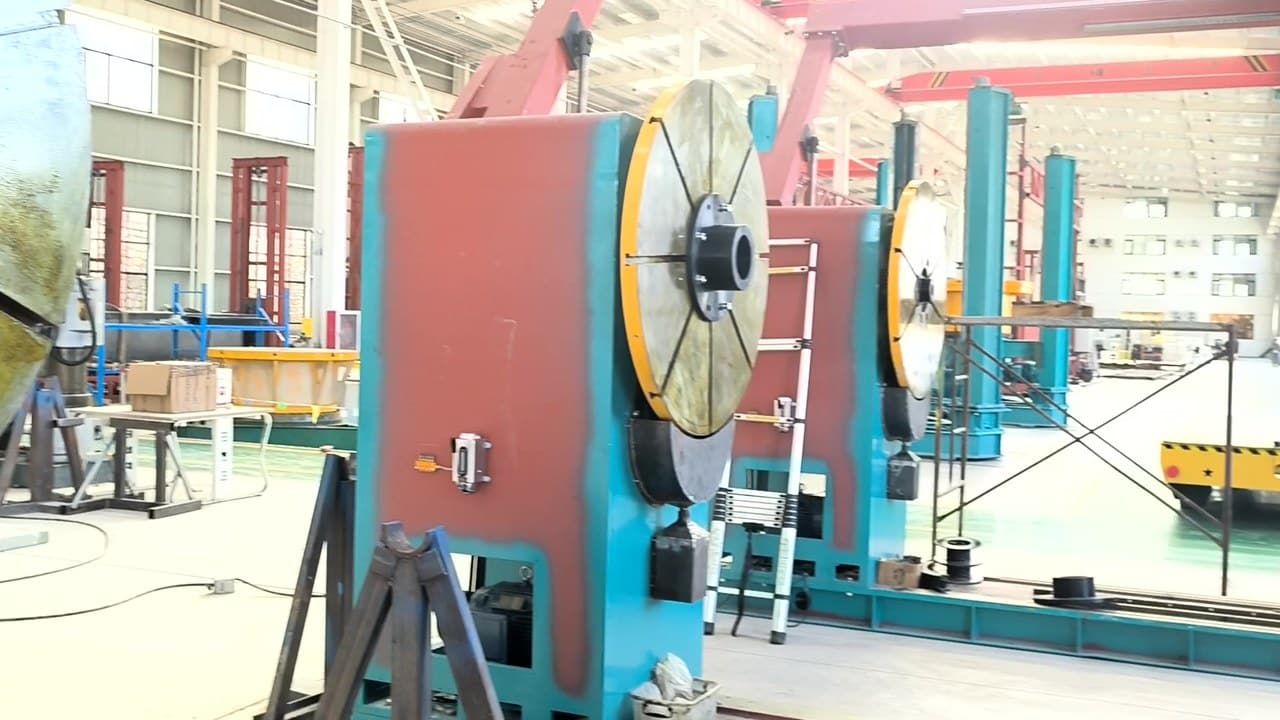
Horizontal Winding Machine Enables Precision Winding for Large Reactor Coils in Dubai, UAE
Reactor winding challenges, machine selection, and four-month results: coil cycles from 2.5-3 days to 1.5-2, start-up shock displacement eliminated.
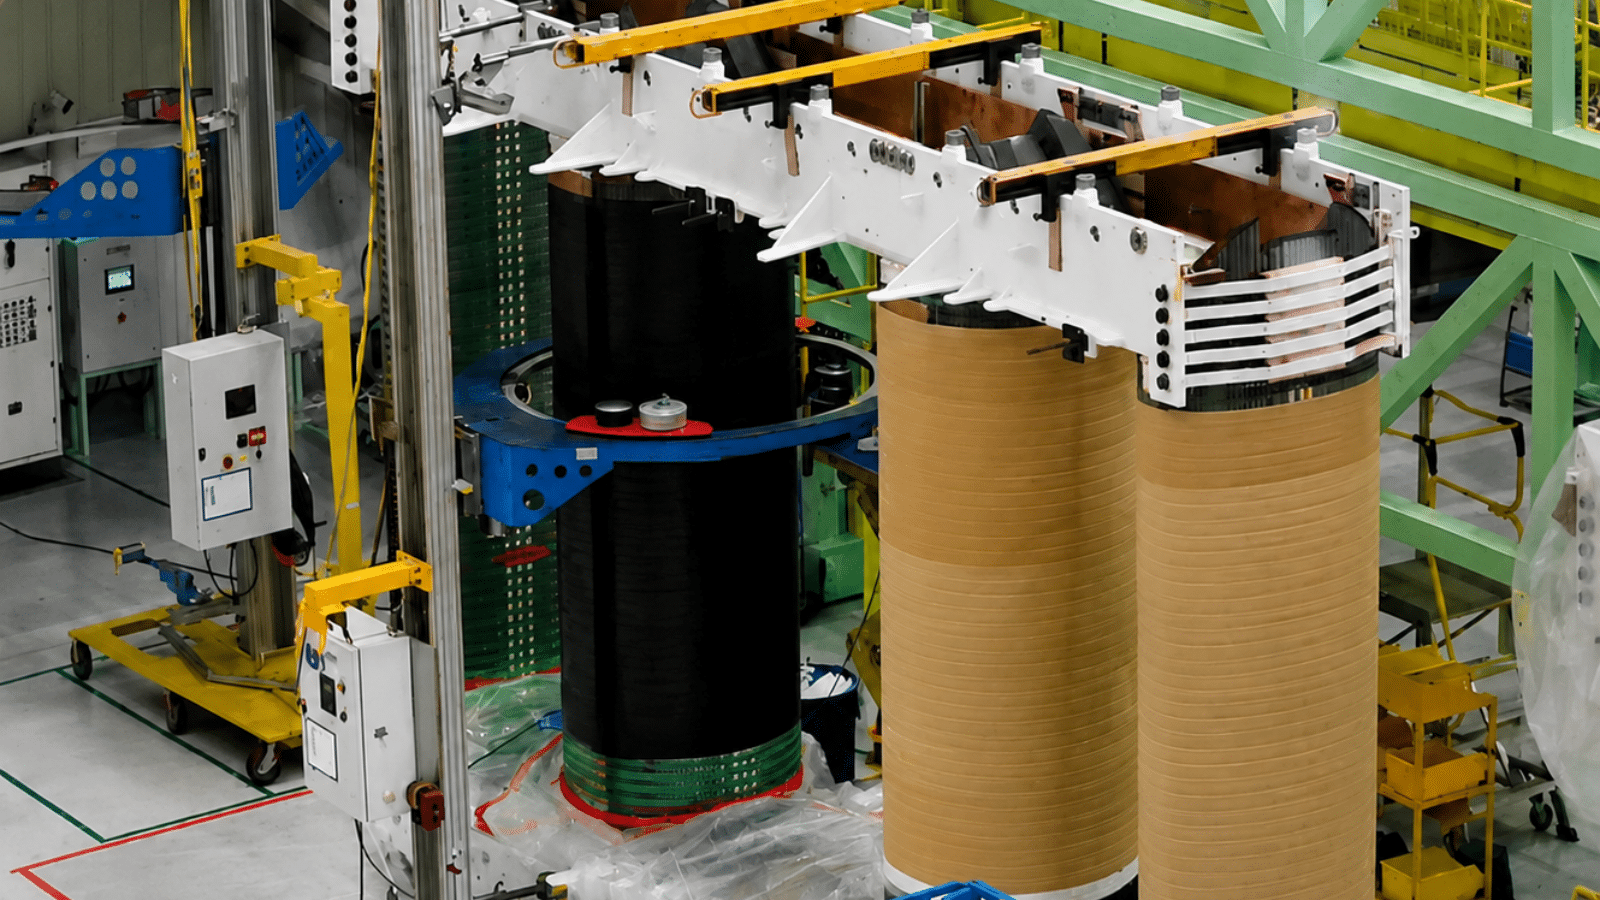
Iron Core Binding Machine Case Study: Ontario, Canada Distribution Transformer Manufacturer
Manual binding pain points, commissioning process, and results: cycle time from 4-6 hours to under one, tension consistency, ~15% less waste.
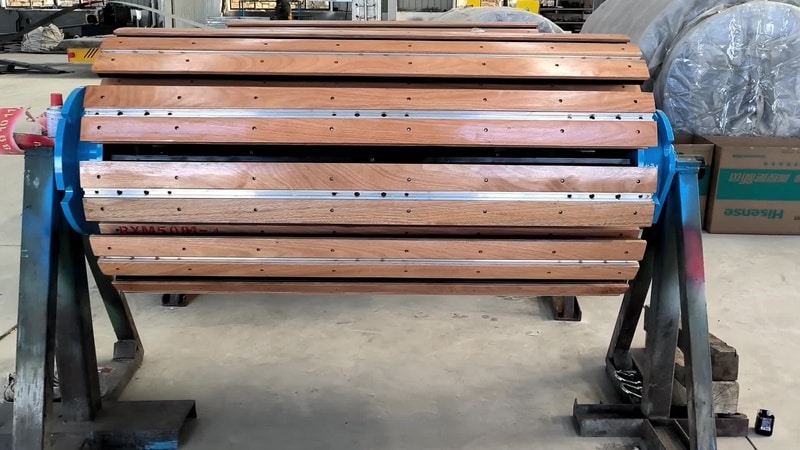
Old fixed-mandrel problems, machine selection, and six-month results: changeover in 15-20 minutes, six mandrels replacing twenty, damage under 0.5%.
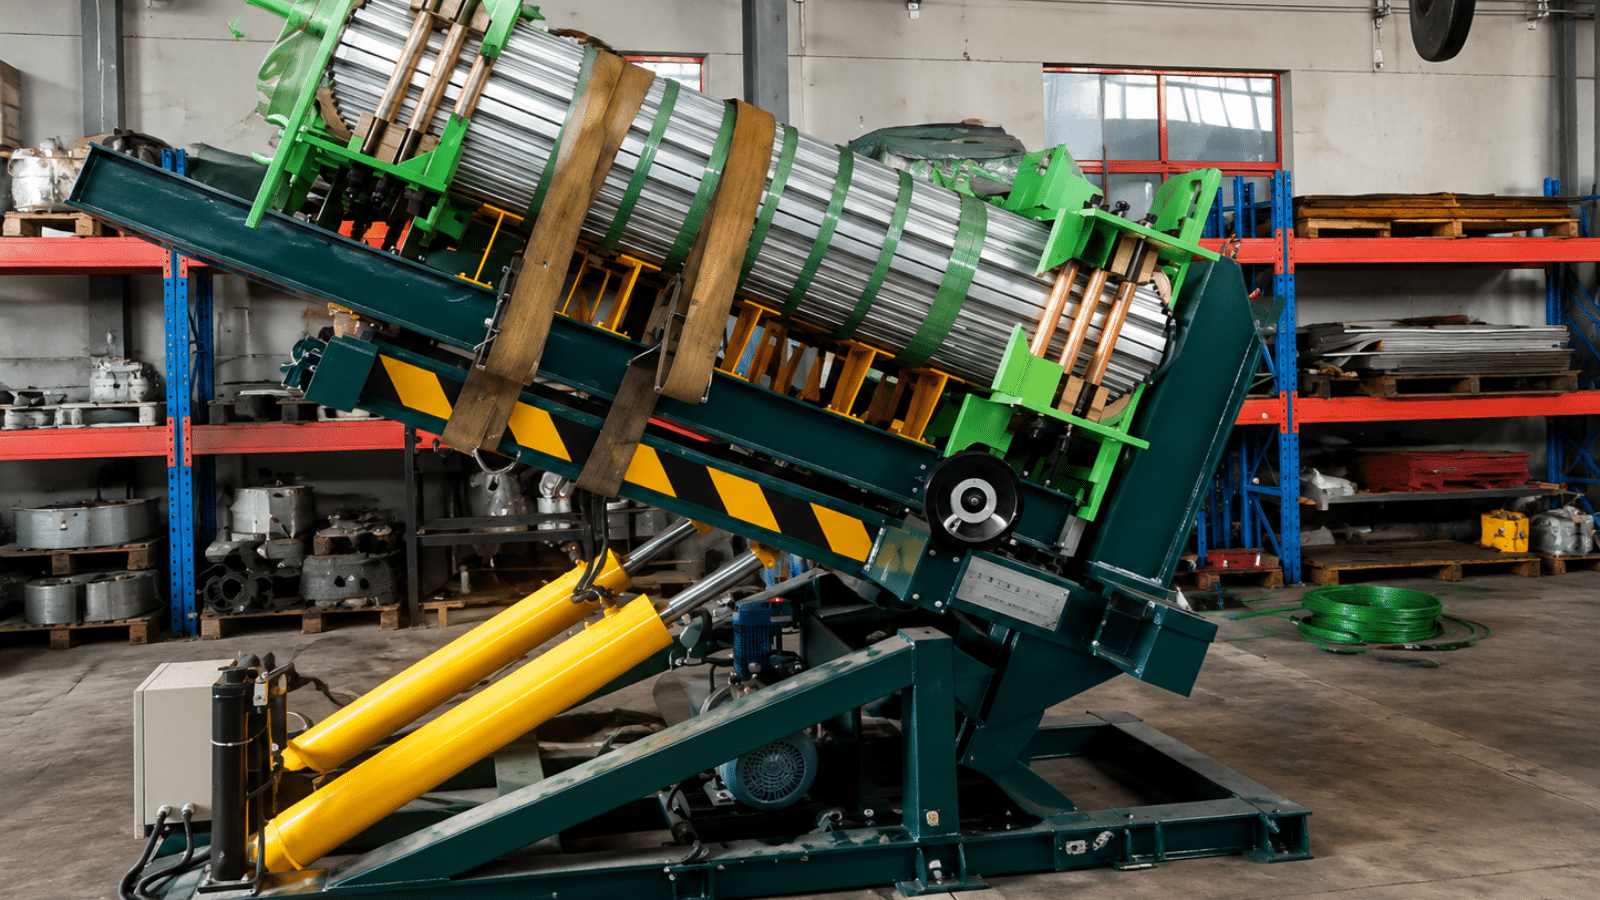
Transformer Core Stacking and Turning Table for a Brazilian Power Transformer Manufacturer
How integrated stacking and 90-degree turning replaced separate stations and crane lifts: one move per core, distortion under 3 mm, no civil-work pit.

