
Die changes and re-clamping were the bottleneck. One die library plus six-axis servo runs a 15×200 mm bar end to end in one clamping at ±0.2 mm.
TRANFOVIA(NINGBO) EQUIPMENT TECHNOLOGY CO.,LTD

Die changes and re-clamping were the bottleneck. One die library plus six-axis servo runs a 15×200 mm bar end to end in one clamping at ±0.2 mm.

See how an Indian transformer and switchgear manufacturer combined busbar sawing and hydraulic folding in one CNC machine for copper bars up to 260 × 6 mm.

See how a South Korean transformer manufacturer automated oil duct curtain production with ±0.5 mm pitch accuracy and output up to 50–100 spacer strips per minute.
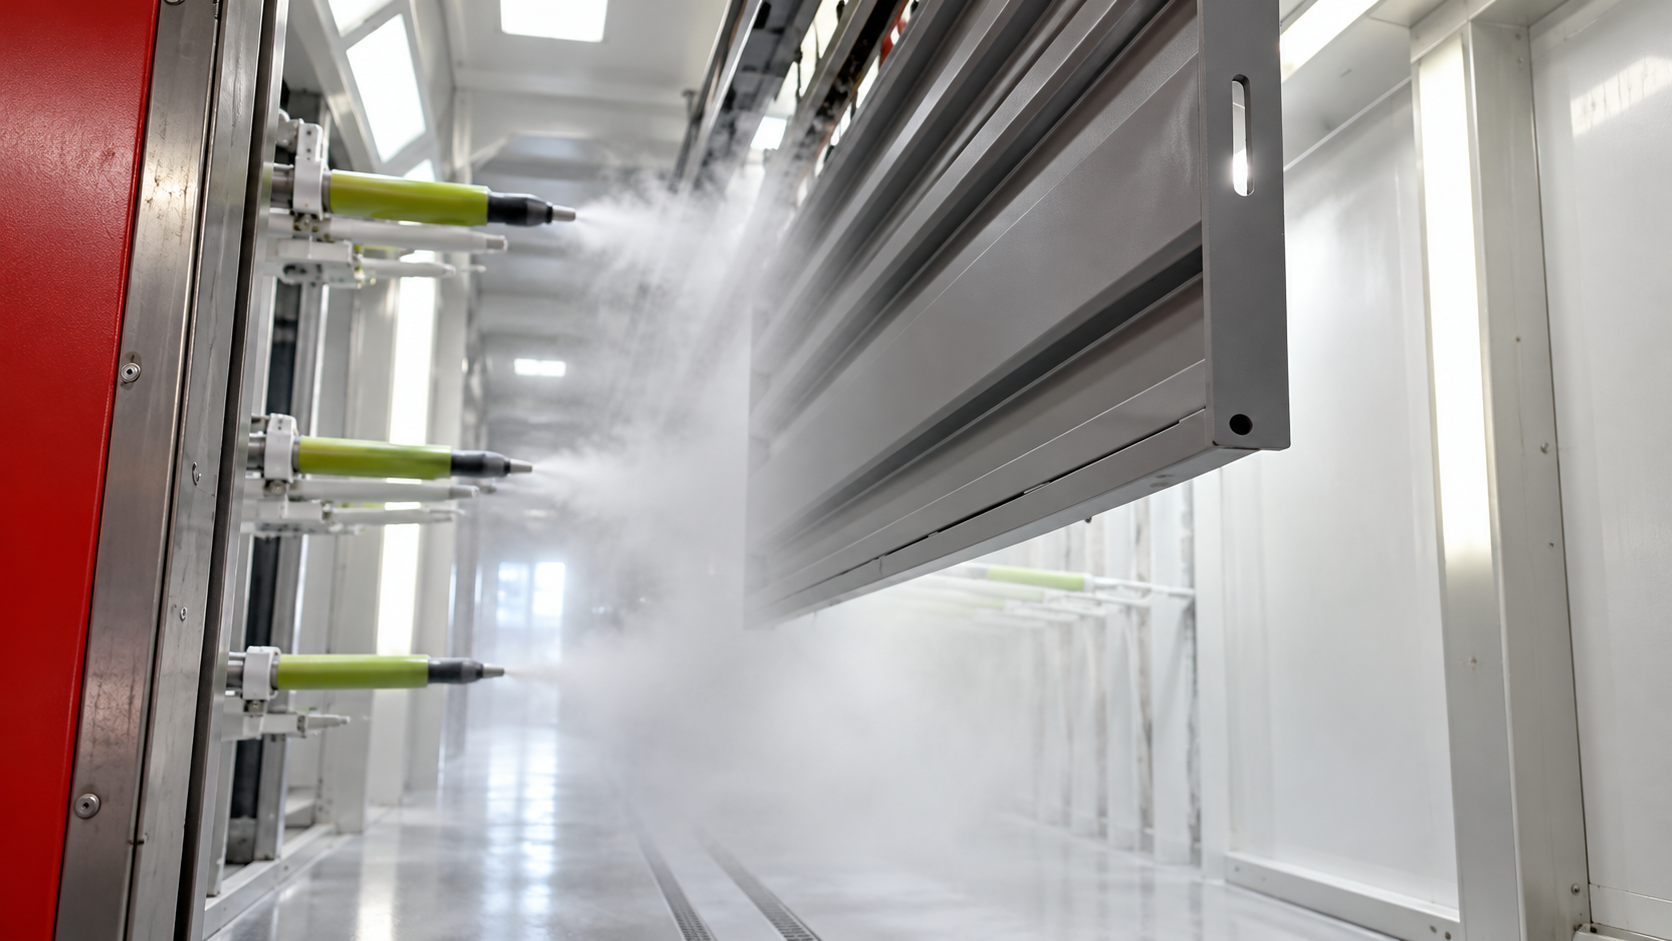
See how TRANFOVIA supplied an automatic powder coating line for transformer tanks in India with 8 electrostatic guns, 95% cyclone recovery and controlled curing.
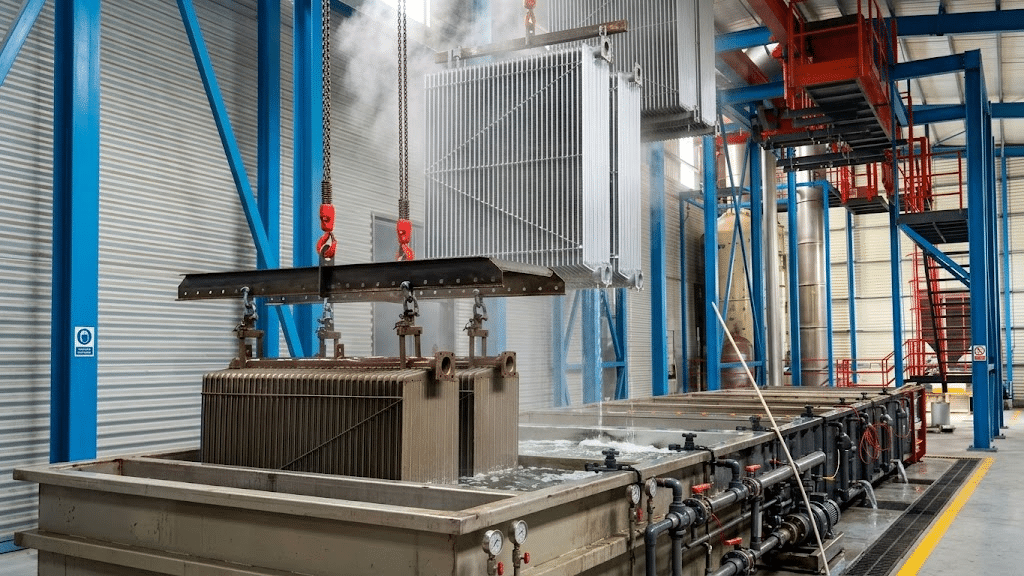
Sri Lanka manufacturer improves transformer tank coating with Tranfovia’s gantry immersion line, delivering 200h+ salt spray resistance.
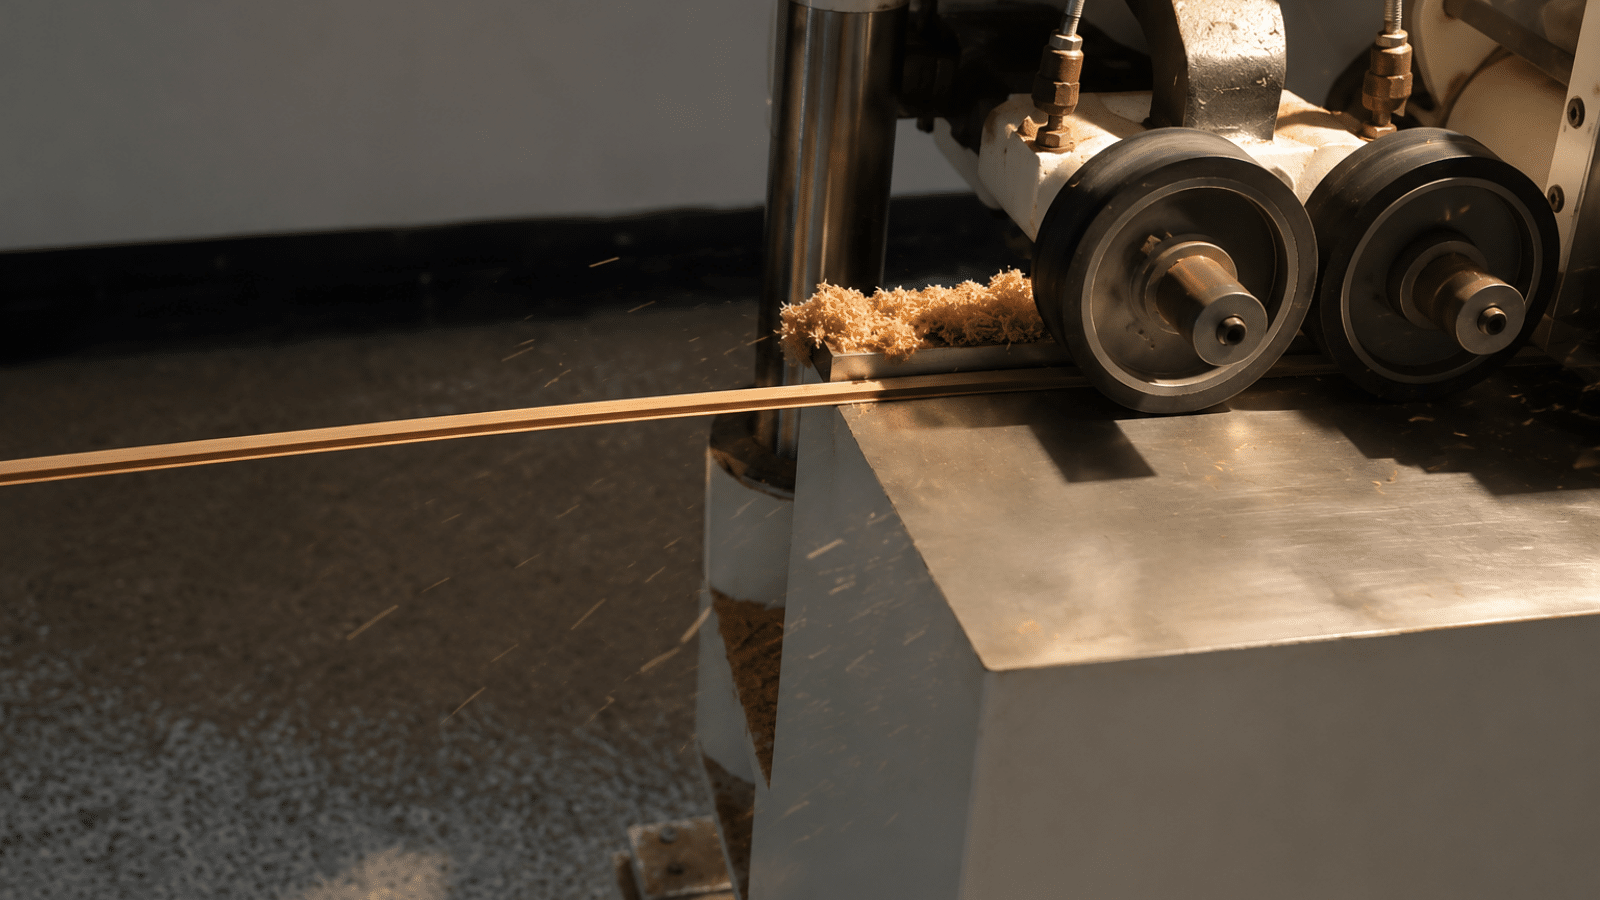
Rolling and chamfering ran as two steps with hand-finished R edges. One pass now holds an 8-10% ratio and clean edges on 1.5-15 mm strips.
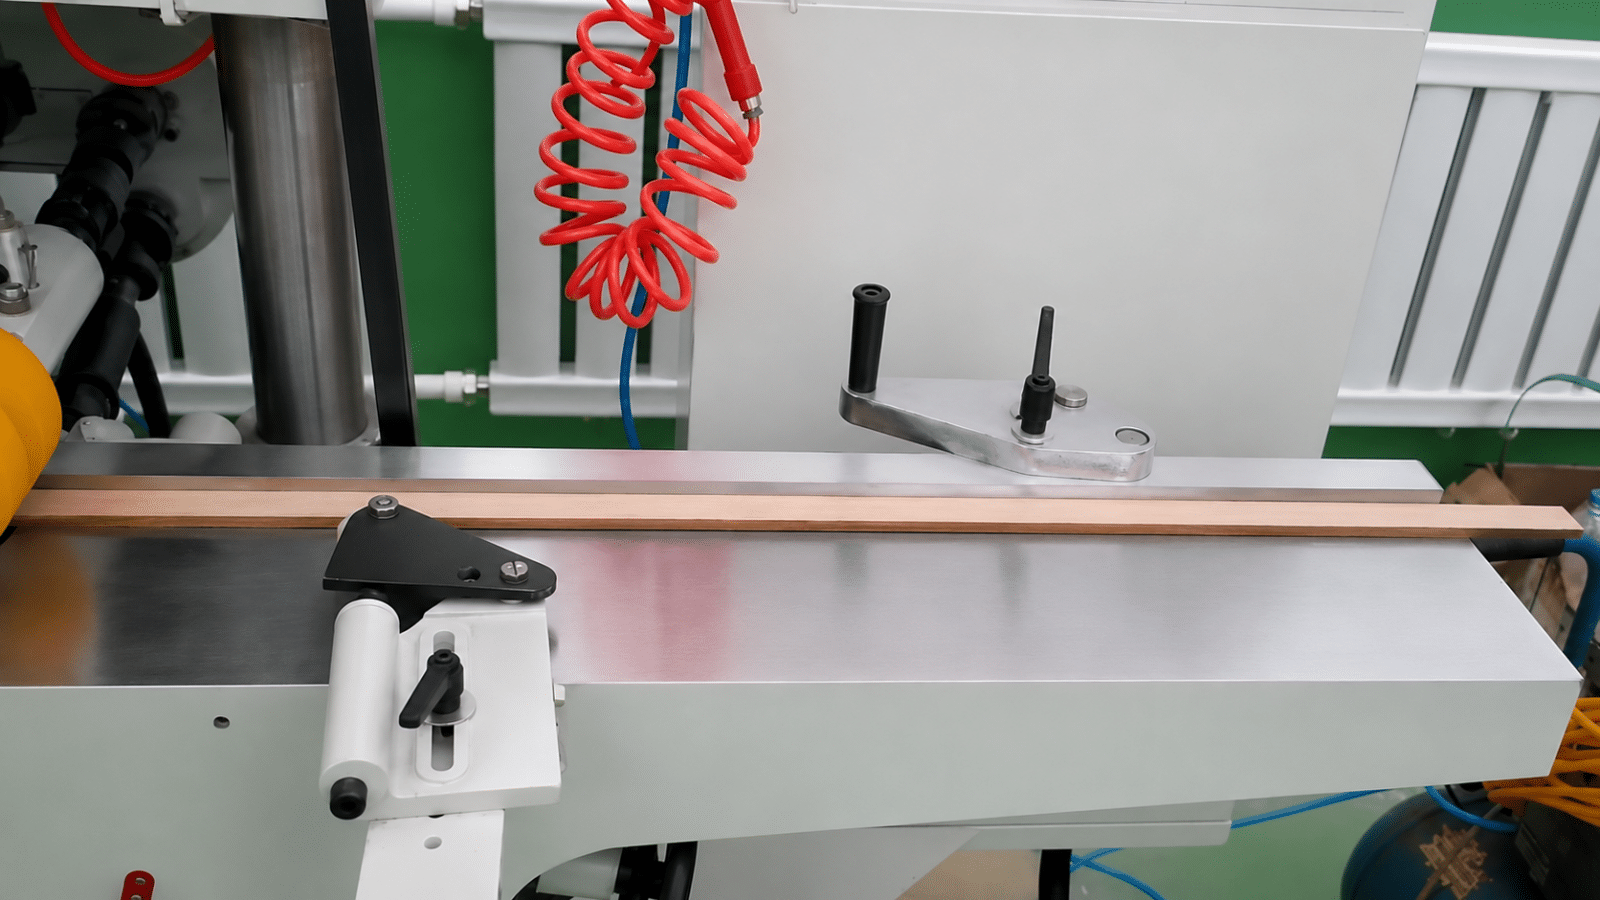
Four profiles needed four methods and wide strips over 70 mm were outsourced. One cutter shaft now runs 10-100 mm T-type and oil-gap strips.
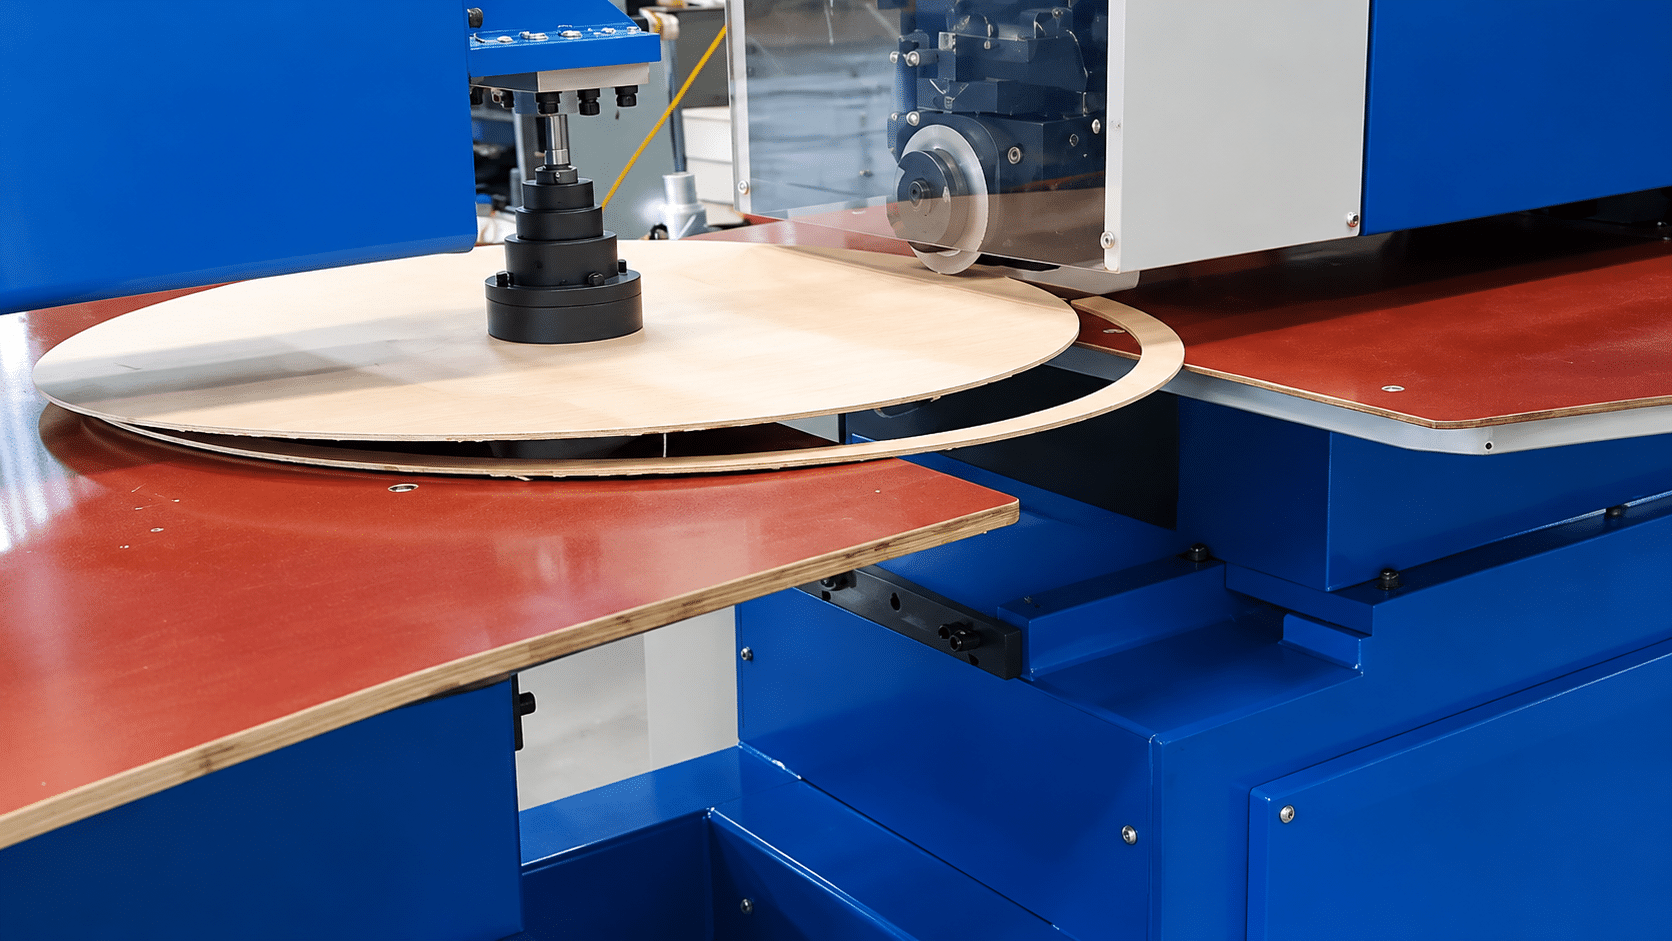
Subcontracted rings took 4-6 weeks and hand cutting drifted ellipticity. Supports hold a 2.8 m sheet at +/-1 mm; one rotation shears a clean ring.
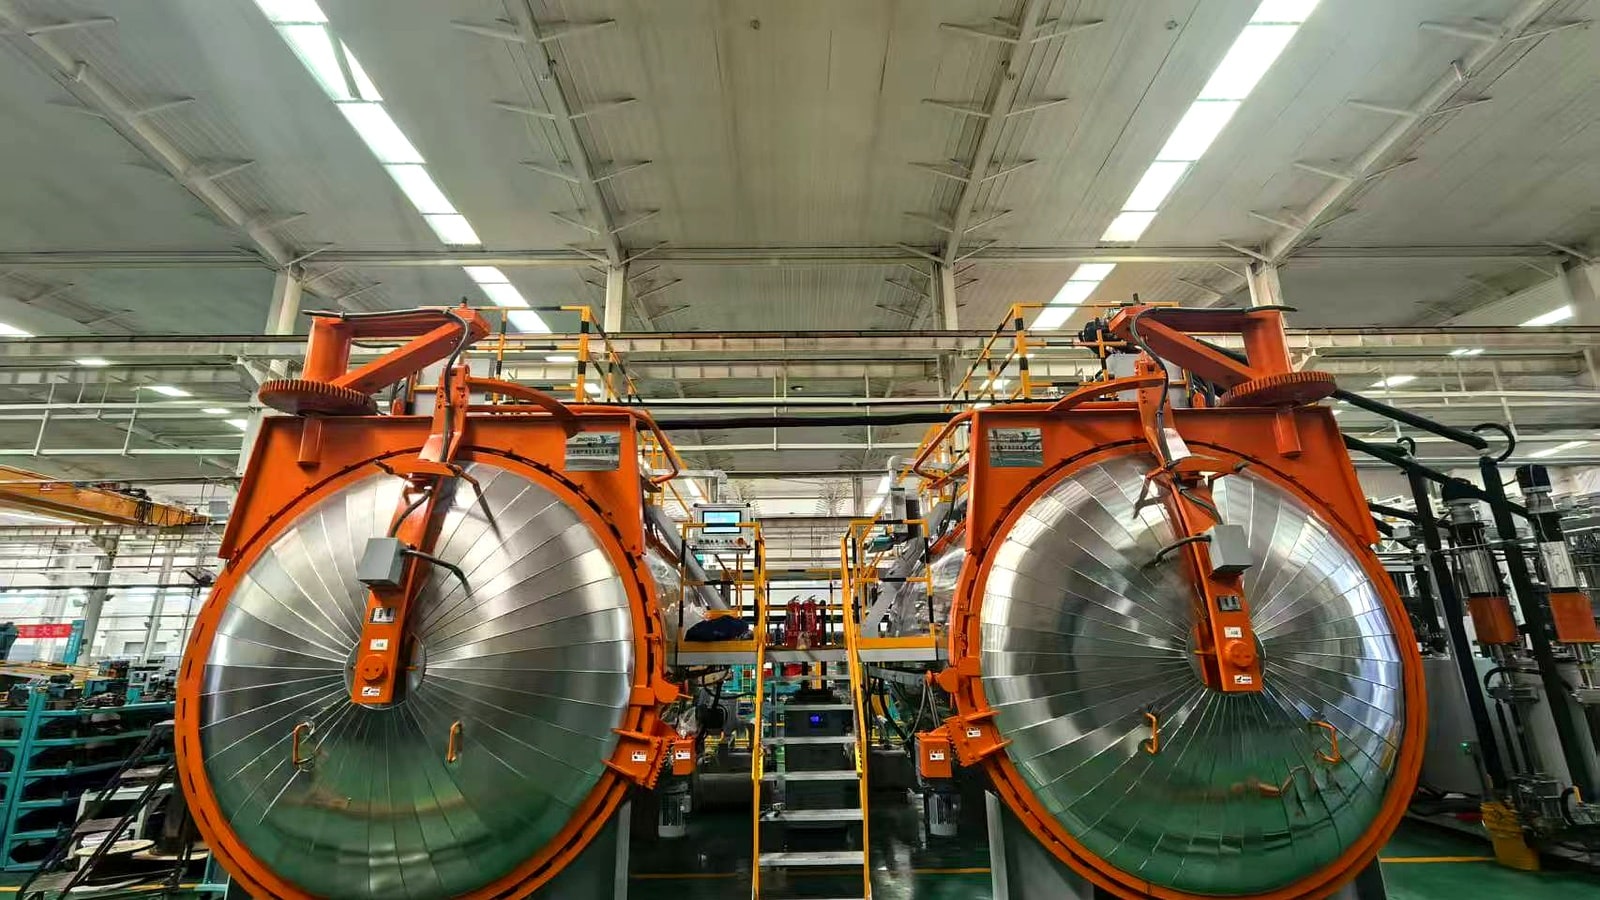
Batch mixing hit pot-life limits and hand weighing drifted. Static mixing now prepares material at the pouring head, 9,000 kg/24h continuous.

