
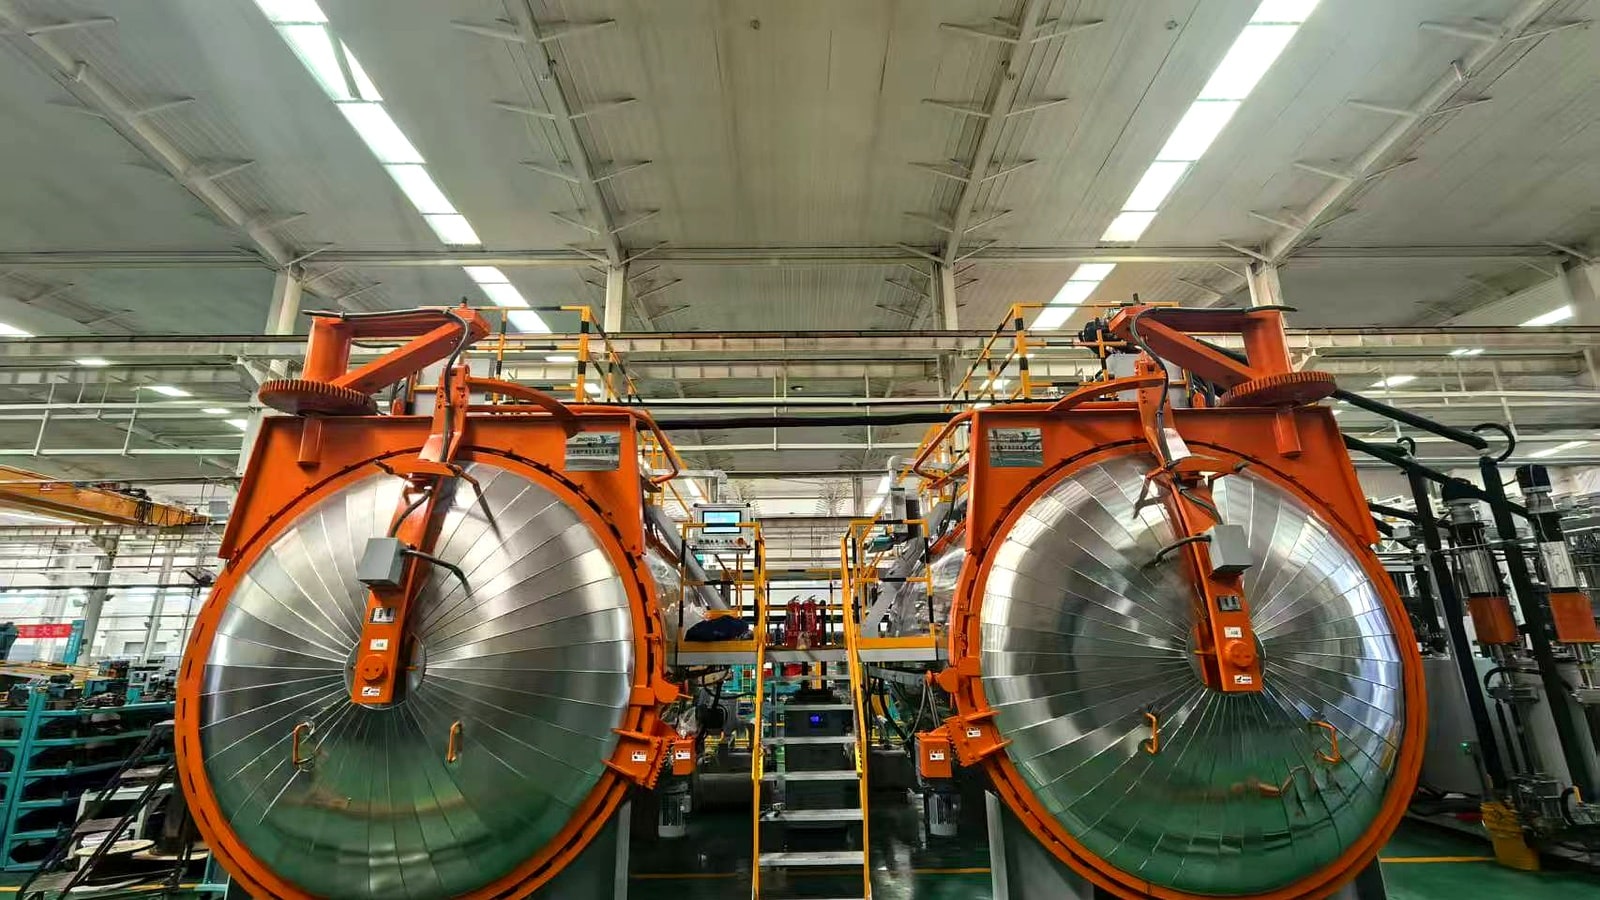
| Equipment | Static Mixing Vacuum Casting Equipment (100–500 L tank range, square or round vacuum pouring box) |
| Customer | An instrument transformer (CT/VT) and small reactor manufacturer in Quito, Ecuador (South America market) |
| Application | Epoxy vacuum casting of current transformer, voltage transformer and small reactor coils, with material preparation, static mixing, vacuum pouring and parameter recording running as one continuous process |
1. Customer Background
This customer is based in Quito, Ecuador and builds current transformers, voltage transformers and small series reactors for local distribution and industrial projects. Its product range is wide and its batch sizes are small, and casting had always run on an older vacuum casting tank with manual material preparation: epoxy, hardener and silica filler were weighed to the recipe, tipped into the tank, stirred, and poured until the batch was used up. Whatever was left when the pot life ran out was drained and the tank washed out. With many part numbers in the schedule, the shop changed material several times a day, and every change meant weighing, pulling vacuum and cleaning the tank — so the shortest part of the day was the pouring itself. When the customer expanded capacity, it placed the order for this static mixing vacuum casting equipment.
2. Industry Pain Points
Casting a CT/VT or reactor coil is both an insulation and a mechanical operation, and the condition of the resin decides whether the part comes out with voids or partial discharge. The customer’s original method carried six problems:
- Pot life set the schedule. A full tank was mixed at once, then sat in the tank waiting for parts. Once the pot life expired the whole batch was scrap, and the more part numbers in the day, the more was thrown away.
- Hand weighing drifted the ratio. Epoxy, hardener and filler were weighed by hand to a paper recipe, and a little too much or too little hardener moved curing shrinkage and internal stress with it.
- Filler settled in the tank. Silica filler sank while the material stood, so the second half of a tank carried less filler than the first, and parts cast from the same batch did not match each other.
- Pouring speed did not match the part. Thin-wall parts took air when filled too fast, while large housings thickened before they were filled when run too slowly, and the valve was adjusted by feel.
- No process record. Vacuum level, pouring pressure and time lived on a sheet of paper or in the operator’s head, so when voids appeared there was no way back to the tank that caused them.
- Long stops for material changes. A recipe change meant breaking pipe connections, washing the tank and pulling vacuum again, which cut the day into small pieces of usable pouring time.
3. Solution
We configured the system around the customer’s largest single-shot casting weight and its daily material consumption:
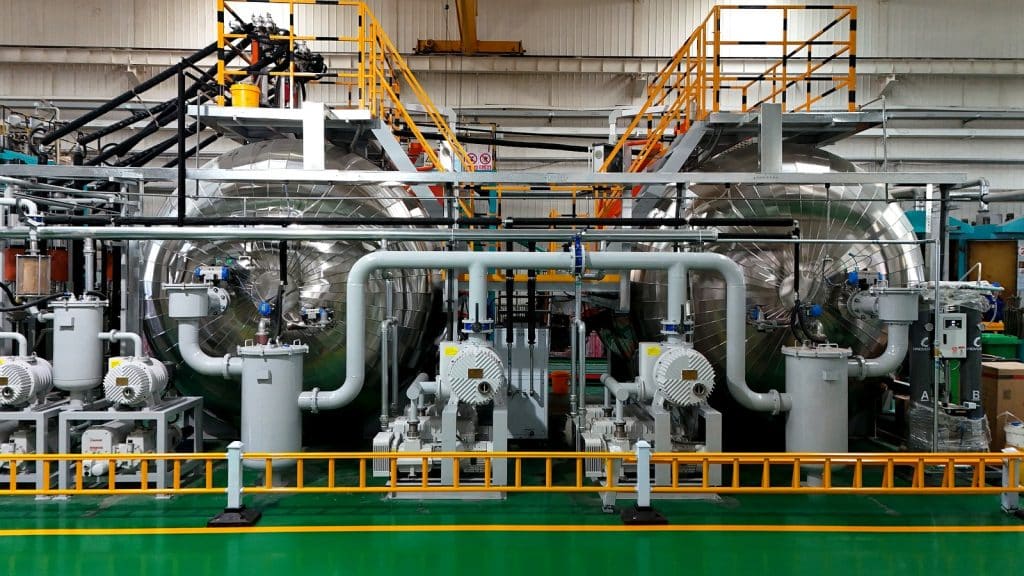
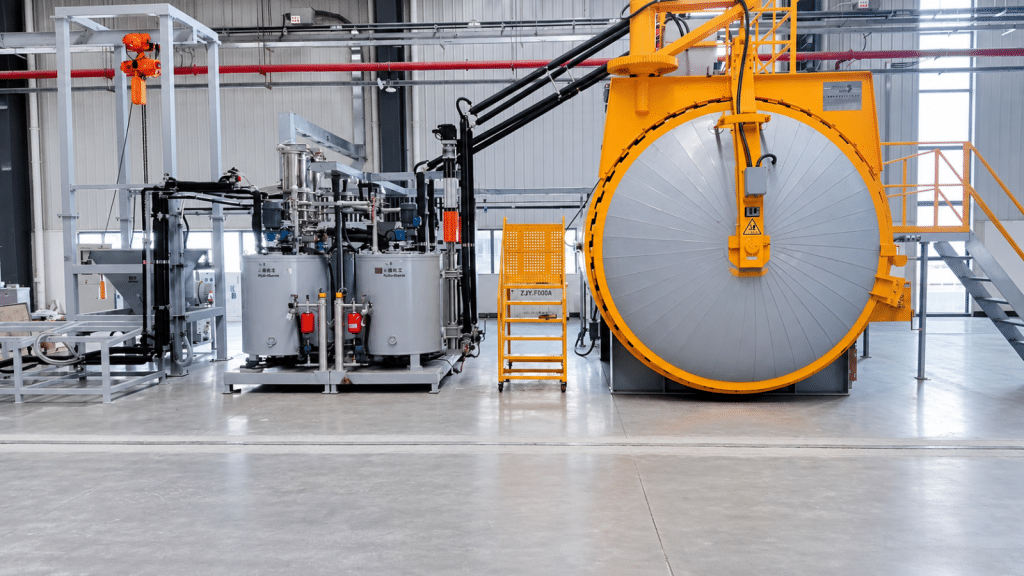
- Mixed at the point of use. Static mixing takes place at the outlet, so epoxy and hardener only meet in the short section ahead of the pouring head. No mixed material is stored in a tank, and material is prepared in the quantity the next parts need.
- Continuous preparation with self-mixing. A 300 L tank runs with 9,000 kg/24h of material preparation, so the system prepares while it pours. The customer compounds its own material to its own ratio, which keeps material cost out of a pre-mixed supplier’s price list.
- Separate filler drying and metering. A 900 kg packing drying tank holds the silica filler dry and feeds it in proportion, which limits both moisture pick-up and the filler variation that settling used to cause.
- Square vacuum pouring box. The pouring box runs at -0.1 to 0 MPa, so the part is filled under vacuum; maximum pouring pressure is about 10 bar and maximum pouring speed is 6 kg/min.
- Two-axis servo pouring arm. The arm is programmed to the position of each part, running thin-wall parts slowly and housings faster, so different part numbers on the same recipe each get their own path.
- Full parameter recording. Preparation, vacuum level, pouring pressure and time are recorded automatically and stored by batch, so an abnormal part can be traced back to the curve that produced it.
4. Implementation and Commissioning
After the equipment arrived, TRANFOVIA engineers worked through three steps with the customer’s casting shop. First, recipe and selection review: the largest single-shot casting weight and the daily consumption of the current transformers, voltage transformers and small reactors were checked against tank volume and preparation speed, and the 300 L tank, 9,000 kg/24h preparation rate and 900 kg filler tank were confirmed to cover the daily output; the pouring box cavity and the travel of the two-axis servo arm were checked against the customer’s part layout and mould heights; and the two-component and filler connections were confirmed to suit the customer’s existing formulation. Second, site work and dry running: foundation, lifting route, vacuum pump, cooling water and air supply were confirmed, and a dry run verified pouring box sealing and vacuum level, material circuit circulation, each axis of the servo arm, and emergency stop and interlock behaviour. Third, trial casting and acceptance: the customer supplied two current transformer types and one small reactor, parts were cast to the recipe, casting appearance and weight consistency were sampled, the parameter record for every mould was checked for completeness and traceability, and operators were trained on material preparation, tank washing and daily checks from the English operation and maintenance manuals.
5. Acceptance Results
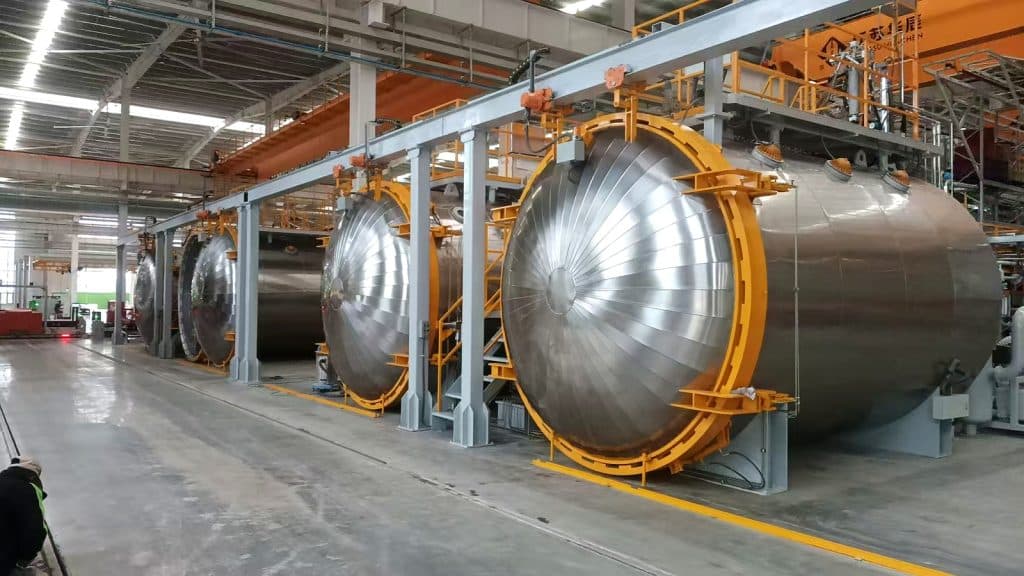
The equipment was verified item by item against the technical agreement. Key parameters are listed below (design and acceptance reference values; actual figures depend on the configuration ordered):
| Parameter | Listed options | Configuration supplied |
| Tank volume | 100 / 150 / 200 / 300 / 500 L | 300 L |
| Material preparation speed | 3,000–15,000 kg/24h | 9,000 kg/24h |
| Packing drying tank | 300 / 600 / 900 / 1,200 kg | 900 kg |
| Maximum pouring speed | 2 / 6 / 12 kg/min | 6 kg/min |
| Maximum pouring pressure | About 10 bar | About 10 bar |
| Pouring box | Square -0.1 to 0 MPa / round -0.1 to 0.6 MPa | Square -0.1 to 0 MPa |
| Pouring arm | Rotary / two-axis servo | Two-axis servo |
Three part numbers ran back to back on the day of trial casting with no stop to drain and clean the tank: the material circuit kept preparing, mixing happened only ahead of the pouring head, and the next mould did not wait for a fresh batch to be compounded. Every sampled casting came out free of surface voids and short fills, weights from the same batch sat in one band, and the vacuum level, pouring pressure and time of each mould matched its part number in the record. Compared with the old whole-tank method, a part number change no longer requires washing the tank and re-compounding.
6. Customer Feedback
“What used to frighten us was a model change: once a tank was mixed we had to keep pouring, and whatever was left was scrap. Now the material is prepared as we need it, a part number change does not mean washing the tank, and the parameters record themselves — when a customer asks about a batch, we can look it up.” — Customer casting shop supervisor (at acceptance)
7. Summary and Next Steps
The value of static mixing vacuum casting equipment is not that it casts under vacuum, but that it turns material preparation from a batch into a continuous flow: mixing happens only ahead of the pouring head, no mixed material sits in a tank, and pot life stops being a constraint on the schedule; continuous preparation and self-mixing hand both material cost and throughput back to the customer; the square pouring box and the two-axis servo arm give parts of different wall thickness and height their own filling curve; and full parameter recording is what makes “why this batch was good” repeatable instead of anecdotal.
Next, the customer plans to turn the recipes and pouring curves of its common part numbers into a process library that is called up by part number, and to add a second unit of the same series when the second expansion phase starts, to take the small-batch orders. To configure a vacuum casting solution around your CT/VT and reactor range, contact the TRANFOVIA technical team for selection advice and a quotation.
- WhatsApp: +86-15958243831
- Email: sales@tranfovia.com
- Website: https://tranfovia.com/




