
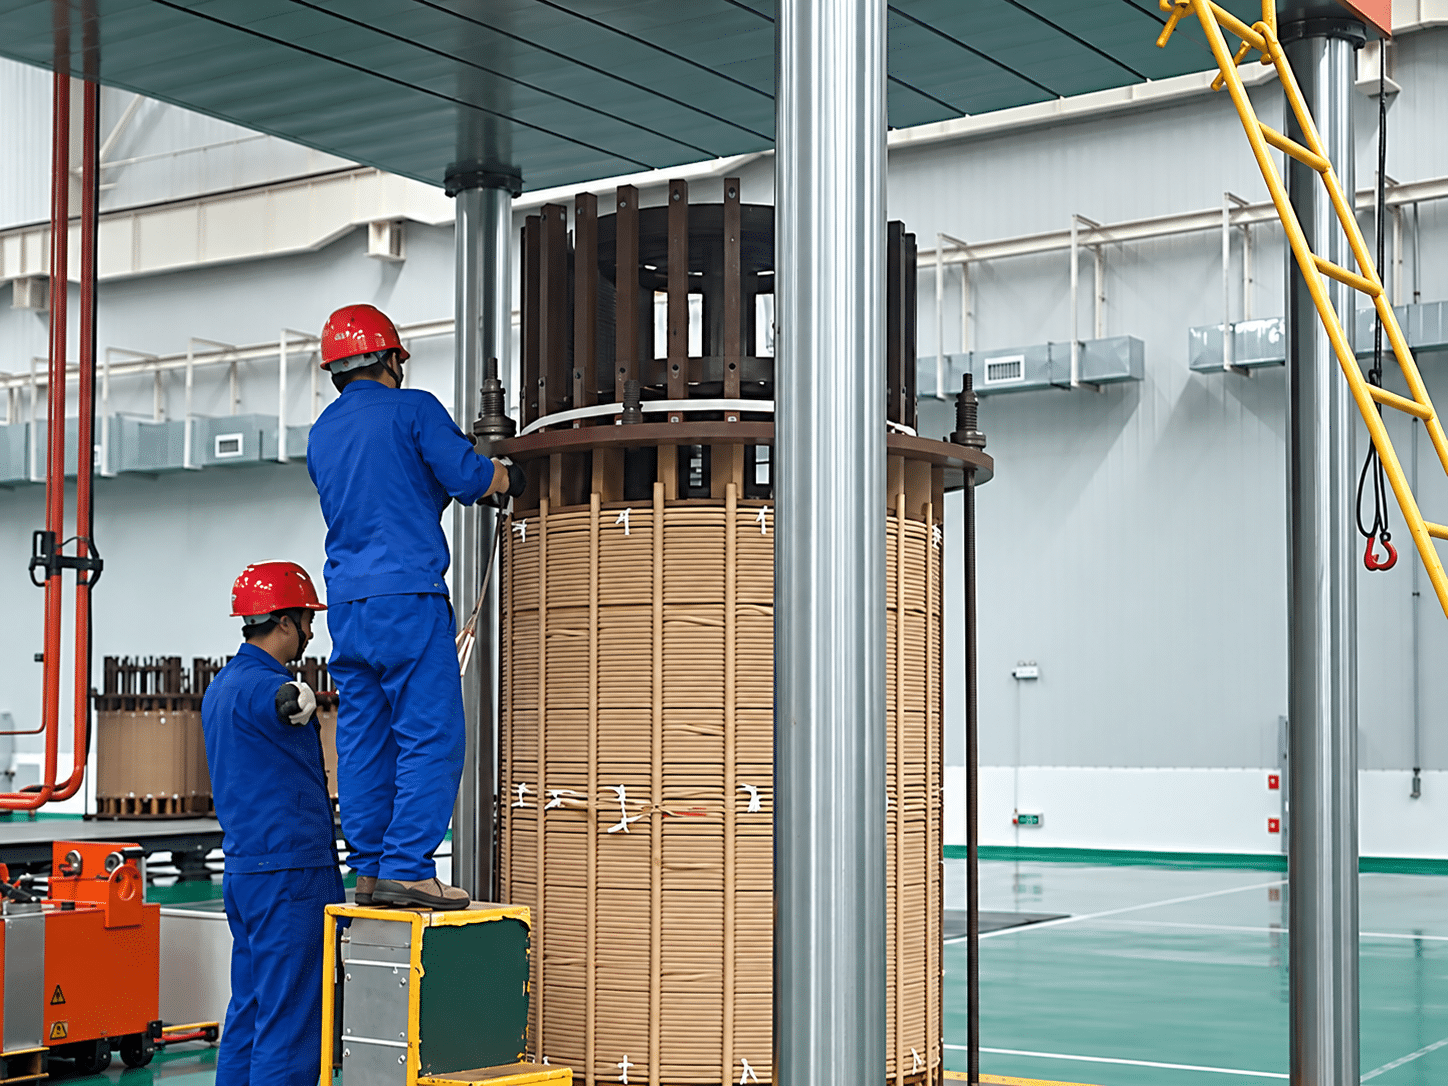
| Equipment | Transformer Coil Press Machine |
| Customer | A power transformer manufacturer in Istanbul, Turkey (serving the European and Middle East utility markets) |
| Application | Axial compaction, multi-spec changeover, and height stabilization of oil-immersed power and distribution transformer coils |
Customer information has been anonymized; only regional and industry attributes are retained. Performance figures represent typical reference values under standard operating conditions and may vary depending on actual production line conditions.
The Challenge: High Mix, Small Batches, and Coils Compacted Only by a Generic Press
Based in Istanbul, this manufacturer produces distribution and medium-size power transformers, a large share of which go to grid and industrial projects across Europe and the Middle East. What makes its coil shop difficult is the high mix and small batch sizes — capacities range from dozens of kVA distribution units to several hundred kVA power units, so coil diameter and axial height vary widely. The shop needed to compact coils reliably while switching between specifications quickly.
Previously, the customer used a generic hydraulic press for coil compaction: press once, measure with a ruler, then add shims. On a multi-spec line, this revealed clear weaknesses:
- Inconsistent height. Across different specs and operators, coil axial height often varied by more than ±4 mm. Coils were either too tall to fit the core window or too loose and needed shim stacking.
- Slow changeover. Changing tooling, adjusting pressure and re-positioning on a generic press often took over 20 minutes per spec. With many small batches, changeover time exceeded the pressing time itself.
- Weaker short-circuit resistance. A winding with residual internal voids can be displaced by axial electromagnetic forces during a short circuit — one of the most common failure modes of oil-immersed transformers.
- Dependence on senior operators. How much force, how long to hold, and how thick the shim all depended on feel, so quality varied with the person running the press.
- A line bottleneck. Repeated pressing, measuring and shimming took nearly half an hour per coil, slowing the whole production line.
The Solution: A Four-Column Press Built Around Coil Compaction
After evaluating several suppliers, the customer chose the TRANFOVIA transformer coil press machine supplied by us. It is not a general forming press but a machine purpose-built for axial winding compaction, and each structural element answers a specific pain point:
- Four-column hydraulic structure. The pressing load is contained within the machine frame, giving even pressure distribution and reducing the foundation-strength requirement — it fits directly on an existing workshop floor.
- Adjustable top hydraulic cylinder. Axial force is applied from the upper cylinder and set against an approved pressure curve per coil spec, making the pressing cycle repeatable and traceable instead of dependent on feel.
- T-slot upper platen. Pressing tooling for different coil diameters can be mounted and adjusted quickly, cutting changeover time on a high-mix line.
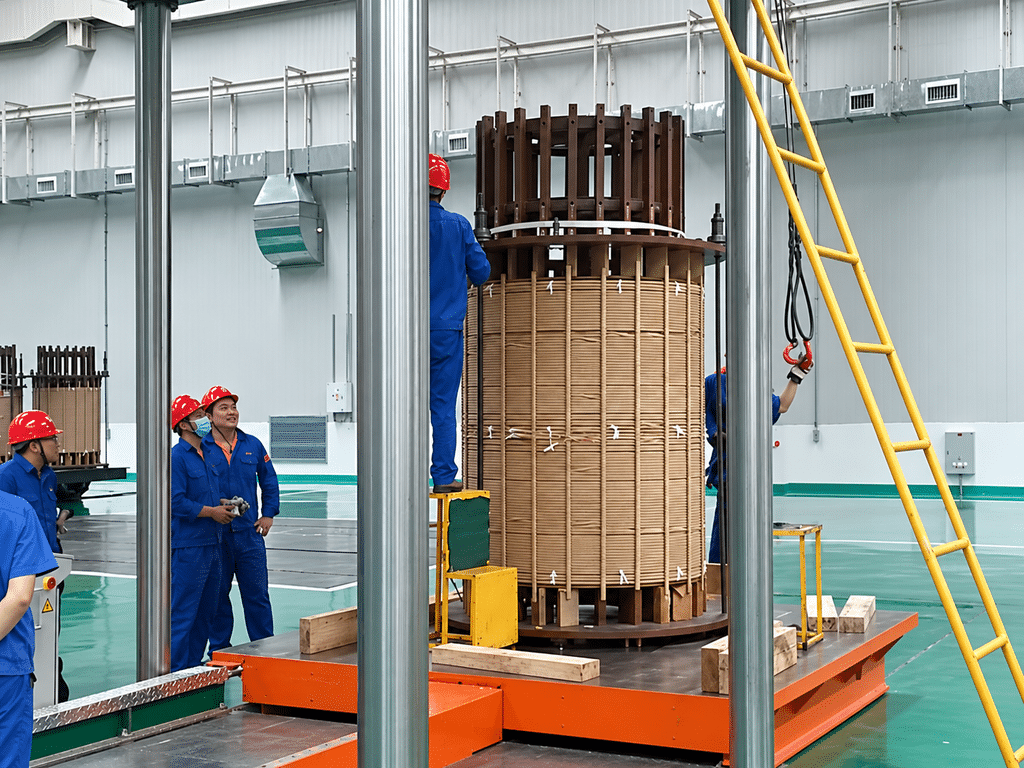
- Motor-driven flat car with automatic positioning. The coil is loaded onto the mobile table, which drives into the pressing station by motor — removing repeated crane positioning inside the machine.
- Concentric centering reference slots. Circular grooves on the flat car give operators a visual reference for placing the coil at the pressing center, preventing off-center loading and uneven pressure distribution.
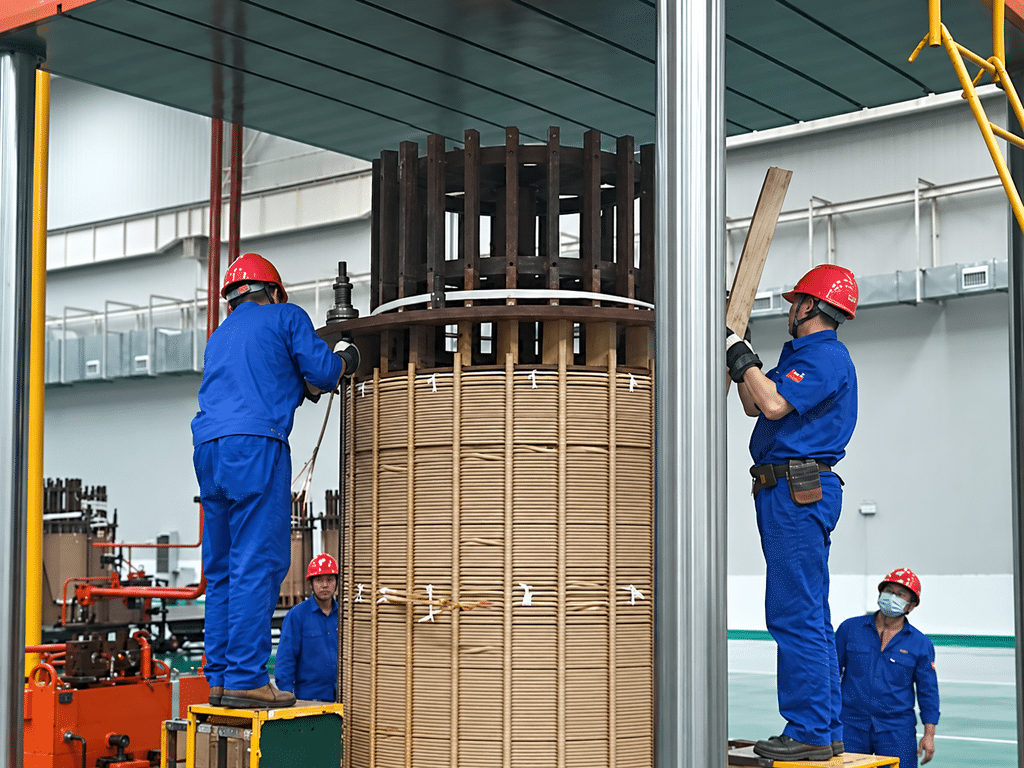
Implementation: Bilingual Manuals, Remote Commissioning, and On-site Guidance
After delivery, we followed our standard export service flow: supplied English/Turkish bilingual manuals and operator training videos, completed installation and pressure-parameter calibration remotely with our engineers, and ran acceptance via remote video; we then dispatched an engineer on site to guide first-piece pressing and lock the pressure and hold-time values for each coil type onto a process card. The customer reorganized the workflow into a defined sequence: coil off the winding machine → load onto flat car → center on reference slots → program-based pressing with hold time → height measurement → record on the process card → release to the drying stage. A per-spec “parameter changeover” standard was also established.
The Results: Consistent Heights, Faster Changeover, Sturdier Windings
Once in production, the customer reported clear improvements (figures shared by the customer; results may vary by application):
| Metric | Before | After |
| Coil height consistency | ±4 mm or more | within ±1.2 mm |
| Pressing time per coil | 28+ minutes | ~10 minutes |
| Multi-spec changeover time | 20+ minutes | ~5 minutes |
| Pressure control | Manual, experience-based | Programmed by process, recorded |
| Core assembly rework | Frequent on-site shimming | Mostly first-time fit |
Just as important, the first-attempt pass rate in short-circuit type testing improved noticeably once the windings were compacted to a denser, more consistent structure. Scheduling across the high-mix line no longer stalls at the coil shop. The customer’s production lead commented:
“Changing specs and pressing coils used to depend on the feel of senior operators, and with many batches it got chaotic. Now pressing follows a program and changeover follows a standard: heights are consistent, throughput is up, and we hold our delivery promises to customers in Europe and the Middle East more reliably.”
Why Customers Choose Us
- Purpose-built for coils. Four-column hydraulic structure, adjustable top cylinder and motor-driven flat car form a complete solution around winding compaction and multi-spec changeover — not a general press doing an awkward job.
- A fit for high-mix lines. We have long served transformer manufacturers across winding, pressing, drying and assembly, and can recommend a configuration based on your coil envelope, batch size and capacity — not a brochure.
- Export-ready service. English-speaking sales and after-sales support; export packing, sea freight and customs documentation handled end to end. Remote acceptance and on-site guidance are available on request.
Ready to Stabilize Your Coil Pressing and Changeover?
Coil compaction is one of the most underestimated steps in transformer production — it directly determines coil height, short-circuit strength and operating stability. If multi-spec changeover time, height consistency or pressing quality is a concern at your plant, talk to us. We can recommend the right machine configuration and workflow based on your coil specifications and process requirements.
- WhatsApp: +86-15958243831
- Email: sales@tranfovia.com
- Website: https://tranfovia.com/




