Product Introduction
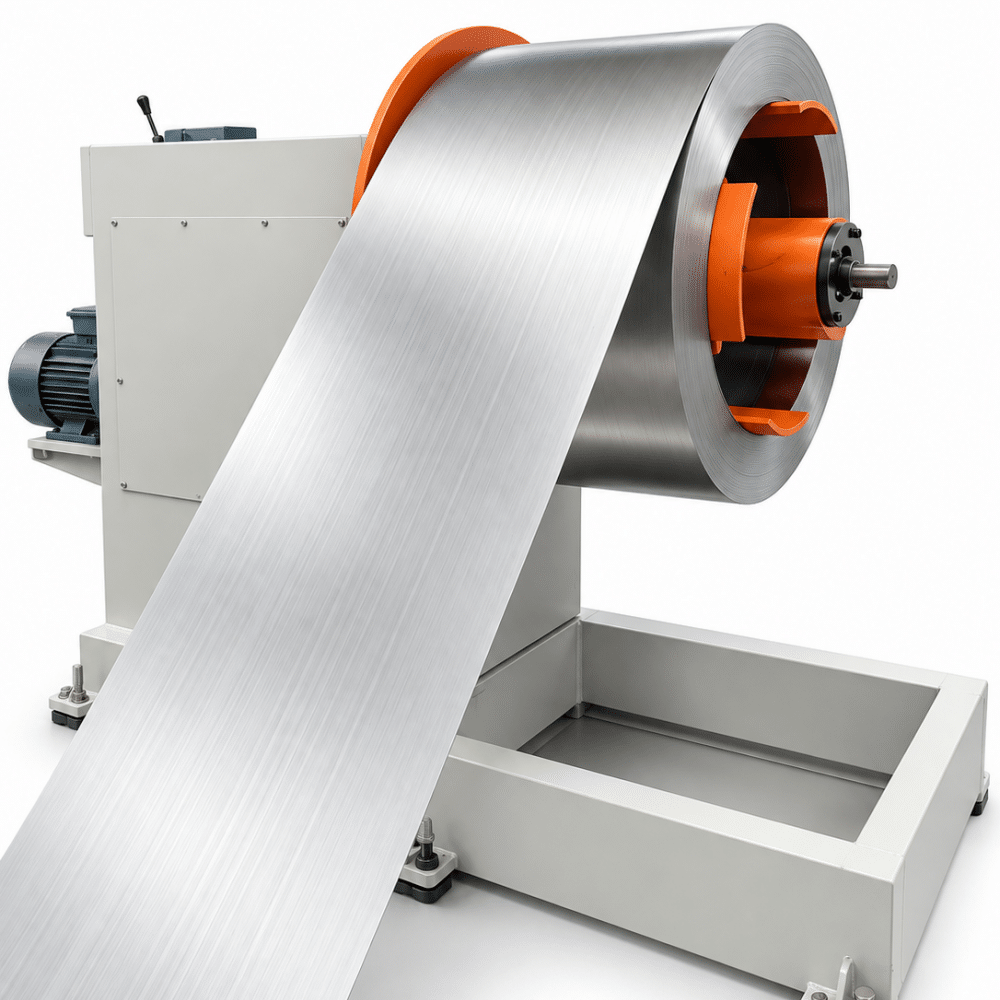
The Transformer Radiator Panel Hydraulic Mandrel Decoiler is the first processing unit in an automatic transformer radiator production line, designed to uncoil and continuously supply steel strips to the radiator panel roll forming machine.
The machine uses a hydraulic expansion mandrel system to securely hold the steel coil and ensure stable unwinding during continuous production.
With automatic tension control and speed synchronization with the forming machine, it provides smooth material feeding, improved forming stability, and consistent radiator panel quality.
This equipment is an essential solution for transformer manufacturers requiring efficient and reliable radiator panel production.
| Max coil weight
5,000 kg (8,000 kg heavy duty) |
Max coil width
545 mm (1,000 mm heavy duty) |
| Coil bore
Ø470 – 520 mm |
Drive / expansion
3 kW motor / hydraulic mandrel |
Main Features
- Hydraulic Mandrel Expansion System
The hydraulic expansion mandrel securely clamps the steel coil, ensuring stable unwinding and reliable material feeding during production.
- Automatic Speed Synchronization
The decoiler works together with the roll forming machine through sensor-based speed control, automatically matching feeding speed with the forming process.
- Stable Coil Tension Control
The system maintains consistent strip tension, reducing material vibration and improving the dimensional accuracy of radiator panels.
The machine supports different coil specifications, with options for standard and heavy-duty models according to production requirements.
- Easy Operation and Maintenance
The equipment supports automatic, manual, and reverse operation modes, providing convenient operation and flexible production control.
Position in Transformer Radiator Production Line
The Hydraulic Mandrel Decoiler is installed at the beginning of the radiator manufacturing process, before the radiator panel roll forming machine.
The typical production sequence is:
Steel Coil Loading → Hydraulic Mandrel Decoiler → Radiator Panel Roll Forming (End Forming / Punching / Cutting) → Panel Turnover & Joining → Multi-Point Welding → Seam Welding → Final Radiator Assembly
During operation, the decoiler automatically expands and clamps the steel coil, then continuously feeds the material to the forming unit according to the required production speed.
Stable coil feeding helps ensure accurate panel forming, reduced material deviation, and continuous automatic production.
Technical Specifications
| Maximum coil outside diameter |
Φ1250 mm (heavy-duty Φ1000 mm / 8 t version optional) |
| Coil inside diameter range |
Φ470 – 520 mm |
| Maximum coil weight |
5,000 kg (heavy-duty up to 8,000 kg) |
| Maximum coil width |
545 mm (heavy-duty 1,000 mm) |
| Motor power |
3 kW |
| Mandrel expansion |
Hydraulic (HOB100 x 150 cylinder) |
| Loop control |
Photoelectric sensor, automatic speed matching |
| Rotation |
Automatic and manual, forward and reverse |
| Foundation |
No pit required |
FAQ
- What is the function of the hydraulic decoiler in a radiator production line?
It securely holds and unwinds steel coils, providing stable feeding before the radiator panel roll forming process.
- How does the hydraulic mandrel system work?
The hydraulic mandrel expands inside the coil, firmly fixing the material and ensuring stable rotation during automatic unwinding.
- What coil sizes can this decoiler handle?
The machine supports coils with Ø470–520 mm inner diameter, up to Ø1250 mm outer diameter, with customized options available.
- What is the maximum coil weight capacity?
The standard model supports up to 5000 kg coils, while the heavy-duty version can handle up to 8000 kg.
- How does the decoiler improve radiator panel quality?
Stable material feeding and tension control help reduce strip deviation and improve the accuracy of subsequent radiator panel forming.
- Can this machine be supplied separately?
Yes. It can be supplied as a standalone hydraulic mandrel decoiler or as part of a complete radiator panel manufacturing solution.