Product Introduction
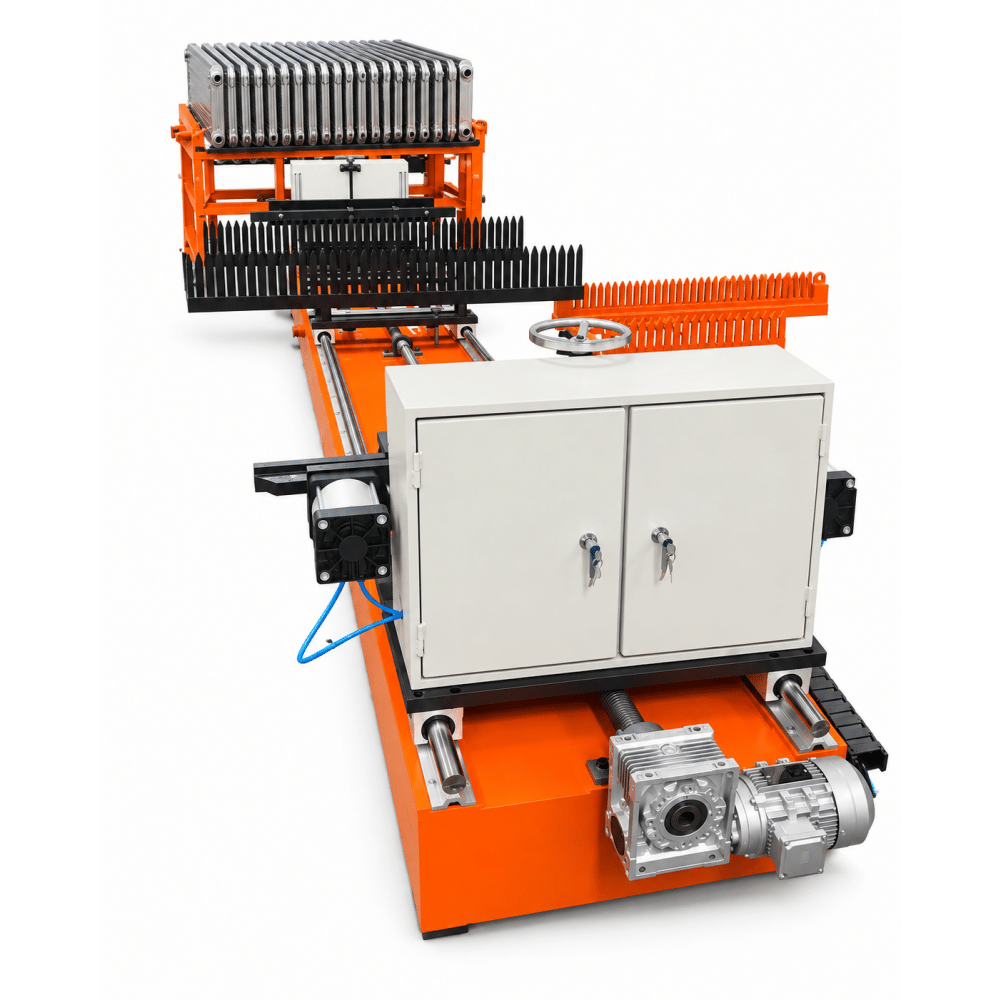
The Transformer Radiator Assembly Fixture is designed for assembling transformer radiator panels into complete radiator banks before header pipe welding.
The fixture accurately positions multiple radiator panels according to preset spacing and provides hydraulic clamping to hold the panel stack and header pipes in the correct position during welding.
With precision locating combs, adjustable panel pitch, and stable hydraulic clamping, the equipment ensures consistent radiator assembly quality and improves welding accuracy.
It is an essential assembly solution for transformer manufacturers producing large radiator banks with multiple panels.
| Base
6,000 × 760 × 190 mm |
Max assembly
4,000 mm |
| Panels per group
up to 40 |
Pitch
45 mm (40 mm option) |
Position in Transformer Radiator Production Line
The Transformer Radiator Assembly Fixture is installed after the automatic stacking process and before radiator turnover and final welding operations.
Typical production process:
Steel Coil Feeding → Hydraulic Mandrel Decoiler → Radiator Panel Roll Forming → Panel Turnover & Joining → Multi-Spot Welding → Dual Seam Welding → Edge Trimming → End Cutting → End Welding → Straightening & Leveling → Automatic Stacking → Header Pipe Assembly
After individual radiator panels are produced and stacked automatically, the fixture organizes the panels into a complete radiator bank.
The fixture controls:
- Panel spacing
- Header pipe positioning
- Welding alignment
ensuring stable assembly before welding.
Key Features
- Accurate Panel Pitch Control
The locating comb maintains consistent panel spacing during assembly.
- Standard pitch: 45 mm
- Optional: 40 mm
This ensures uniform radiator structure and simplifies downstream welding operations.
- Hydraulic Positioning and Clamping
The hydraulic clamping system applies stable pressure along the radiator bank, keeping panels and header pipes accurately positioned during welding.
- Large Radiator Assembly Capacity
The fixture supports:
- Maximum radiator length: 4000 mm
- Maximum panels per group: 40 panels
Suitable for large transformer radiator assemblies.
- Heavy-Duty Base Structure
The fixture uses a robust welded structure with:
- 16 channel steel
- 6 mm steel plate
- 16 mm locating comb teeth
providing sufficient rigidity during assembly and welding.
- Flexible Welding Application
The fixture can be used with:
- Manual tack welding
- Vertical seam welding fixture
according to production requirements.
Technical Parameters
| Base Dimensions |
6000 × 760 × 190 mm |
| Assembly Capacity |
Up to 4000 mm radiator length |
| Panel Capacity |
Maximum 40 panels/group |
| Panel Pitch |
45 mm standard / 40 mm optional |
| Clamping Method |
Hydraulic locating and clamping |
| Welding Method |
Manual tack welding / Vertical seam welding fixture |
| Base Structure |
No.16 channel steel + 6 mm steel plate |
| Locating Comb |
16 mm steel plate cutting structure |
FAQ
- How many radiator panels can be assembled?
The fixture can assemble up to 40 radiator panels in one group.
- What radiator length can the fixture support?
The standard design supports radiator lengths up to 4000 mm.
- What is the standard panel spacing?
The standard panel pitch is 45 mm, with 40 mm optional spacing available.
- Why use hydraulic clamping?
Hydraulic clamping provides uniform pressure along the radiator assembly, improving positioning accuracy and welding consistency.
- What welding process can be used with this fixture?
The fixture supports manual tack welding and vertical seam welding applications.
- Where is this fixture installed in the production line?
It is installed after automatic stacking and before header pipe welding and radiator finishing processes.